Surface Finishing Customization for Manufacturing Parts
Specify what the surface must do: protect the part, control friction, carry identification or meet an appearance reference. A finish must suit the base material and leave critical fits usable. Mark visible areas, contact surfaces and dimensions that must be checked after finishing.
A surface finish is not an afterthought — it is a functional specification
The finish must be specified against the actual material, manufacturing route, appearance target and service environment. Durability, sterilization compatibility, color stability and wear life require project-specific tests and acceptance criteria.
This page compares mold texture, as-machined surfaces and possible post-processing options so buyers can discuss a finish before production. Process availability, the execution route, finish limits, inspection method and any required sample approval are confirmed for the quoted part; the examples below are not a blanket capability or performance guarantee.
Injection Molding Surface Finishes
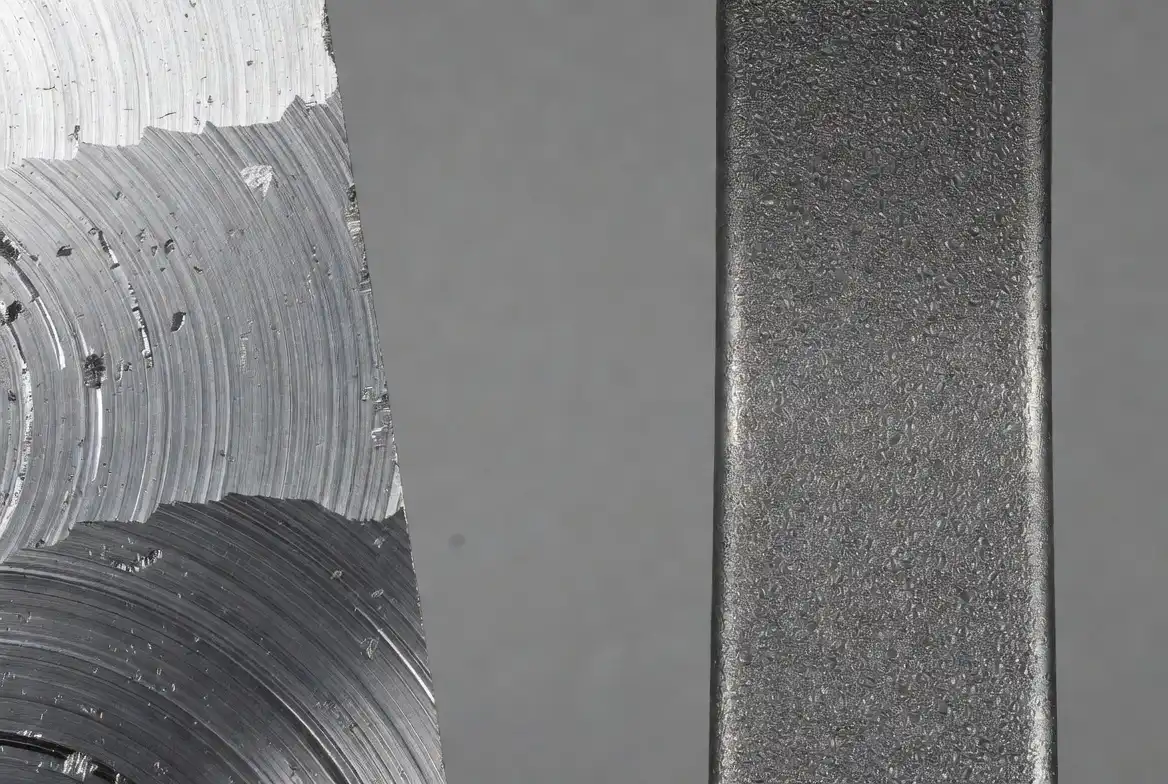
Mold texture and polish can affect the molded part, but replication depends on resin, part geometry and processing. Select a target finish during mold design review, then approve a physical sample against the agreed viewing and inspection conditions. Listed post-mold methods are options to discuss, subject to project confirmation.
| Finish option to review | Material and use | What to confirm before ordering |
|---|---|---|
| Mold polish or texture | Appearance molded into a compatible plastic part | Resin, target surfaces, draft, approved sample and inspection light |
| Printed or decorated graphics | Logos, symbols and labels on a compatible substrate | Artwork, adhesion, cleaning exposure and marking durability |
| Painting or coating | Color or protection where substrate and process permit | Adhesion, coating thickness, masking, exposure and sample approval |
| Laser marking | Part identification or graphics where the material responds suitably | Contrast, readability, location and any traceability standard |
| Metallization | Metal appearance or function on a qualified plastic substrate | Feasibility, adhesion, thickness, conductivity and required testing |
CNC Machining Surface Finishes
CNC surfaces start as-machined. Mechanical, chemical and coating methods are options to assess, subject to material compatibility and project availability. Specify the target Ra and inspection area on the drawing.
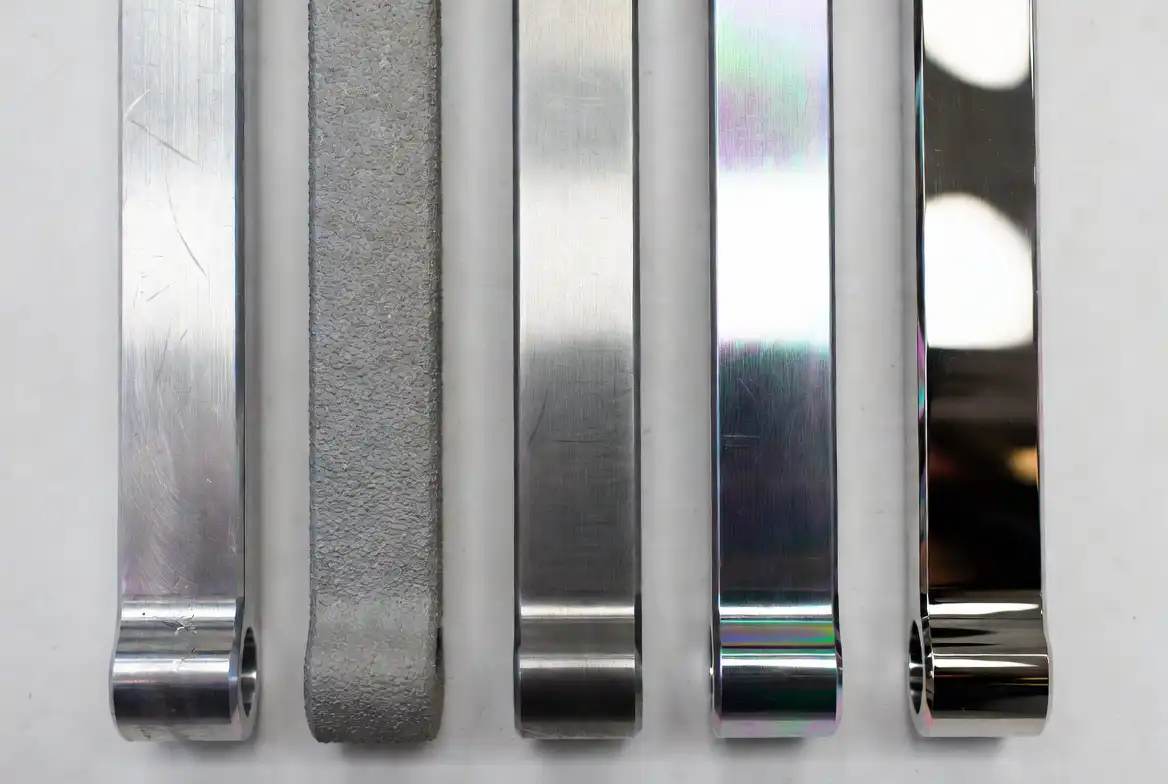
As Machined
Visible tool marks may remain. Specify any critical roughness value and measurement location on the drawing; achievable finish depends on material, geometry and toolpath.
No separate finish stepConfirm target Ra
Bead Blasting
Uniform matte texture by propelling glass beads or oxide media. Masks tool marks and prepares for coating.
Consistent matteDeburrs edges
Anodizing (Type II / III)
Electrochemical oxide layer on aluminum; Type II for cosmetic and general use, Type III for hardcoat wear resistance.
Corrosion resistantColor options
Electropolishing
Electrochemical polishing can smooth selected metal surfaces. Specify material, target roughness and any regulated-use requirements; availability and validation are confirmed for the project.
Target Ra to agreeSample to confirm
Powder Coating
A cured powder coating may provide color and protection on compatible metal parts. Coating thickness, fit allowance, exposure and required tests must be agreed before quoting.
Thickness to agreeColor sample
Brushed & Polished
Mechanical brushing for satin directional finish or progressive polishing to mirror finish. Common on stainless steel and aluminum trim.
DecorativeSample finish to confirm
SPI Mold Finish Groups — Selection Guide
SPI grade labels are a common way to describe a mold-surface target. The groups below are selection directions, not measured results for a quoted tool or part. Specify the target on relevant surfaces and confirm appearance and roughness with samples and an agreed method.
| SPI group | Typical mold-surface direction | Buyer approval point |
|---|---|---|
| A — polished | High-gloss direction | Confirm steel, resin, optical or cosmetic target and molded sample |
| B — semi-gloss | Fine stone or abrasive direction | Confirm visible areas and appearance against an approved sample |
| C — satin | Lower-gloss abrasive direction | Confirm texture, cleaning and visible surface zones |
| D — textured | Blasted or textured direction | Check draft, release, grip and replication on the selected resin |
3D Printing Post-Processing Finishes
Additive parts may show layer lines. The following post-processing options need a material-specific feasibility review and sample approval before they are included in a quote.
Vapor Smoothing
Chemical smoothing may reduce visible layer lines on a compatible printed material. Chemical compatibility, dimensional effect, surface target and availability require a sample review.
Layer-line reductionTest for sealing
Sanding & Priming
Sanding and primer can reduce visible layer lines before painting. Agree the target appearance and check any effect on critical dimensions on a sample.
Paint-readySmooth touch
Metal Plating (3DP)
Metallization is an option to assess for selected printed parts. Substrate preparation, coating adhesion, thickness, conductivity and any EMI target need a project-specific feasibility and test plan.
Feasibility reviewSample approval
Surface Finishing by Industry
Use these examples to define the requirement, not as evidence that a particular process or regulated performance is already approved. Confirm material, finish route and test plan for each project.
How to choose the right surface finish
Use these three filters to narrow down finishes before locking specifications on a drawing or RFQ.
Define the primary requirement
Is the finish cosmetic, protective, or functional? A mirror polish is a cosmetic choice; anodizing is protective; electropolishing may target cleanability when material and regulatory requirements permit. One finish can serve multiple goals — prioritize the most critical one.
Match to material and process
Not every finish works on every material. Aluminum anodizes beautifully; steel does not. Injection molded parts reflect the mold finish; CNC parts may remain as-machined or use a separate finishing step. Check compatibility before committing.
Balance cost, volume, and tolerance
Compare tooling effort with per-part finishing work at the quoted quantity. Coatings and polishing can change dimensions or edge conditions, so mark critical fits and ask for the process allowance in the quote.
What affects a finish quotation?
Cost and lead time depend on the substrate, geometry, selected route, finish area, quantity, inspection and approved sample. A comparative chart cannot replace a project quote.
Identify the substrate
Provide the exact plastic or metal grade and the manufacturing process used for the part.
Mark the target surfaces
Call out appearance, texture or roughness, color, masking, critical fits and exposure conditions on the drawing.
Approve the evidence
Agree the sample, measurement method, acceptance criteria and required records before production release.
Frequently Asked Questions
How do I specify a surface finish on my drawing?
The most reliable way is to include three pieces of information: (1) the SPI/VDI grade or Ra value, (2) the process method expected, and (3) which surfaces need the finish. Example: “SPI B-1 on cavity side only” or “Ra 0.8 µm max, electropolish, all external surfaces.” Callouts like “smooth” or “nice finish” are ambiguous and lead to rework — always use standard grades.
What SPI finish should I use for a clear plastic lens?
A high-polish mold may be a starting point, but optical clarity depends on resin, mold steel, geometry, molding conditions and the viewing standard. Define the optical requirement and approve a molded sample before specifying the finish.
Does anodizing change part dimensions?
Yes, and this catches many first-time designers. Anodizing changes the surface and can affect critical fits. Mark press-fit or bearing features on the drawing and agree coating type, target thickness, masking and final inspection dimensions before production.
Can you match a specific color across different materials and finishes?
Color matching across materials is challenging but achievable within defined tolerances. Anodized aluminum, painted plastic, and powder-coated steel will never be identical under every light source due to different surface physics. Approve a master color sample and agree the viewing light, measurement method, tolerance and batch acceptance plan before production.
Need a surface finish recommendation for your parts?
Send a drawing or reference photo, material, quantity, finish target, critical dimensions, service environment and any required tests. We will review feasible options, sample approval and the project-specific quotation before committing to a process.
We do not sell, trade, or rent your personal data. You can contact us at any time to request, update, or delete your information.