Nylon 6 vs Nylon 66
PA6 vs PA66: the quick engineering answer
PA6 vs PA66 starts with the operating conditions and the approved grade. PA6 is a common starting point for general mechanical parts and cost reviews; PA66 is a candidate when heat and sustained load drive the specification. Neither is an automatic replacement for the other. Compare reinforcement, moisture condition, aging and the actual molded part before approving material supply or tooling.
PA6 vs PA66 property comparison
PA6 (nylon 6) and PA66 (nylon 66 or nylon 6/6) are engineering polyamides. This table gives selection criteria, not a universal grade specification. Numerical acceptance limits must come from the named grade datasheet and your drawing.
| Selection factor | PA6 | PA66 | Purchasing and part approval |
|---|---|---|---|
| Melting behavior | Generally lower melting temperature | Generally higher melting temperature | Melting point is not a continuous-use temperature rating. Request heat-aging and loaded-part evidence. |
| Strength and stiffness | Depend on exact formulation and moisture state | Depend on exact formulation and moisture state | Compare the same test standard, conditioning, temperature and reinforcement; family names do not establish a winner. |
| Moisture and dimensions | Absorbs moisture; dimensional and mechanical effects need review | Also absorbs moisture; dimensional and mechanical effects need review | Define inspection condition and in-service humidity, rather than comparing unrelated water-absorption figures. |
| Glass-fiber or FR grades | Specify the exact PA6 grade, glass content and any FR requirement | Specify the exact PA66 grade, glass content and any FR requirement | GF30 is a filler description, not proof of equivalent shrinkage, heat aging or certification. |
| Molding and tooling | Use supplier drying, melt and mold-temperature instructions | Use supplier drying, melt and mold-temperature instructions | A replacement needs a molding trial and dimensional validation; do not assume the original process or tool compensation transfers. |
| Purchasing comparison | Request a quotation for the defined material and quantity | Request a quotation for the defined material and quantity | Compare accepted part cost, documentation and validation scope alongside resin price. |
How to choose between PA6 and PA66
Choose PA6 when
- Part cost and processing efficiency are primary constraints.
- Good toughness, wear resistance and general mechanical performance are sufficient.
- The proposed PA6 grade has verified performance at the working temperature, load and aging duration.
- A PA6 GF grade already meets the dimensional and structural targets.
Choose PA66 when
- The part needs higher dry stiffness or strength retention at elevated temperature.
- Connectors, brackets or under-hood parts face heat and sustained mechanical load.
- A validated PA66 GF, FR, heat-stabilized or impact-modified grade matches the approval requirements.
- The molding process can control drying, melt temperature and crystallization consistently.
PA6 vs PA66 for common application requirements
| Requirement | Start with | Approval check |
|---|---|---|
| Cost-sensitive housing or general mechanical part | PA6 | Impact, stiffness, dimensional tolerance and humidity exposure. |
| Heat-exposed structural or electrical component | PA66 | Continuous and peak temperature, load, aging, flame rating and electrical requirement. |
| High stiffness or low creep | PA6 GF or PA66 GF | Glass content, fiber orientation, weld lines, warpage and conditioned properties. |
| Flame-retardant component | Exact PA6 FR or PA66 FR grade | Required rating, thickness, color and applicable certification for the named grade. |
| Precision part exposed to humidity | Compare conditioned PA6 and PA66 data | Equilibrium moisture, tolerance stack, conditioning method and inspection timing. |
Processing and mold-design differences
PA66 generally runs at a higher melt temperature than PA6. Both materials are moisture-sensitive before molding, so drying should follow the exact supplier datasheet and be checked with suitable moisture-control procedures. Poor drying can cause splay, hydrolytic degradation and loss of mechanical performance.
- Tooling: allow for grade-specific shrinkage and anisotropy, especially with glass fiber.
- Temperature control: use the supplier’s melt and mold-temperature window; avoid applying a generic nylon setting to every grade.
- Inspection: define whether dimensions are checked dry, after conditioning or after environmental exposure.
- Regrind and residence time: agree the limits before qualification when mechanical or appearance consistency is critical.
PA66 grades and real datasheet evidence
PA66 GF10, GF15, GF20, GF25, GF30, GF35, GF40 and GF50 are separate formulations. Flame-retardant versions are also listed separately. Do not copy a GF30 value into an unfilled, GF50 or GF30 FR specification.
For PA66 material selection
Use the PA66 properties and grades guide to define the base resin, reinforcement and operating condition.
For PA66 GF30
Review the PA66 GF30 Datasheet in the verified download library, then request the exact grade document and applicable certificate with the quotation.
WanHan is the manufacturer of the supplier datasheets in that library; Nylon Plastic supports material selection and supply review. The available project documentation can include the grade datasheet, a batch-specific certificate of analysis, and applicable RoHS, REACH or UL documentation where the selected grade and project require it.
Can PA6 Replace PA66 in an Existing Mold?
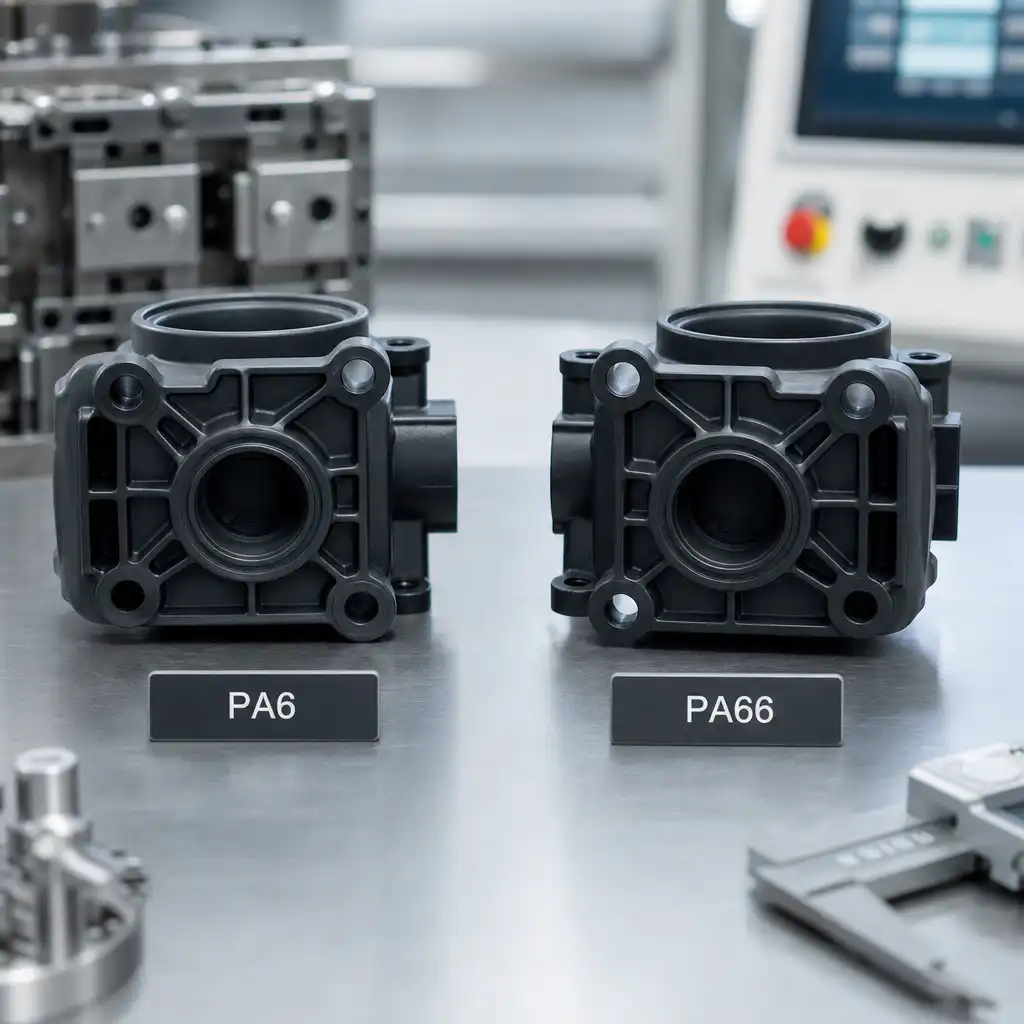
Start with the currently approved grade and the reason for replacement: availability, cost, performance or a specification change. Matching glass content alone does not establish interchangeability.
- Compare grade evidence. Record supplier and grade, color, reinforcement, test standard, dry or conditioned state, required flame rating and document revision.
- Check the real failure modes. Review creep under load, heat aging, impact, fluids, weld-line strength and humidity-driven dimensional change against the application.
- Validate the tool and process. Trial the proposed grade with its supplier processing instructions. Measure critical dimensions, warpage, appearance and assembly fit in the agreed inspection condition.
- Approve the part before the production order. Agree sample acceptance and traceability. A satisfactory datasheet comparison does not replace the molded-part test.
What to Compare in a PA6 vs PA66 Quotation
Nylon Plastic can review the material and manufacturing scope together. The useful output is a proposed grade or route, the evidence still needed for approval, and a quotation based on the defined scope. Tooling, conditioning, inspection, packaging and delivery should be stated explicitly; no material-family comparison establishes a fixed price or lead time.
Manufacturer reference: BASF Ultramid polyamide product overview identifies PA6 and PA66 families and grade-dependent melting behavior. Use the offered grade TDS for purchasing limits; this reference does not imply BASF grade availability from Nylon Plastic.
PA6 vs PA66 FAQ
Is PA66 always stronger than PA6?
No. PA66 often has higher dry stiffness and heat capability, but grade formulation, reinforcement, moisture condition, temperature and part design can reverse a simple material-family comparison.
Which absorbs more moisture, PA6 or PA66?
Both are hygroscopic. Published values depend on test method, exposure and conditioning state, so compare the exact grades under the same test conditions and design around in-use moisture.
Can PA6 GF30 replace PA66 GF30?
Sometimes, but not by name alone. Compare tensile and flexural data, heat aging, impact, shrinkage, moisture response, flame rating, surface requirements and the molded part test.
What should I send for a material review?
Send the drawing or CAD, load, working temperature, humidity or chemical exposure, tolerance, annual volume, color, required certifications and any currently approved material.
Related PA66 and nylon engineering guides
- What is PA66? Properties, grades and applications
- PA66 GF30 material guide
- Nylon moisture absorption and dimensional effects
- Nylon injection molding services
- PA6 vs PA66 vs PA12 comparison
Request a PA6 vs PA66 Material and Part Review
Send the information that changes the decision. The technical team can match the resin family, reinforcement and manufacturing route before quotation.
Drawing/CAD revision, critical dimensions and tolerance; for a prototype, identify appearance, fit or functional testing.
Load, temperature, humidity and chemical exposure.
Approved grade or TDS, or PA6/PA66 requirements; reinforcement, color and required documents.
Prototype/order and annual quantities, sample approval requirements, destination and target timing.