Moving a plastic part from prototype to production requires more than a working sample. A 3D-printed or CNC-machined prototype can confirm shape, fit or a specific function, but it does not automatically prove how the intended production resin will behave in a mold or whether dimensions will repeat. This guide follows the decisions from sample evidence through material and process review, tooling, molded trials and approval. Nylon Plastic can review these connected requirements from the drawing; the route is confirmed for the actual part.
What Does the Plastic Prototype Actually Prove?
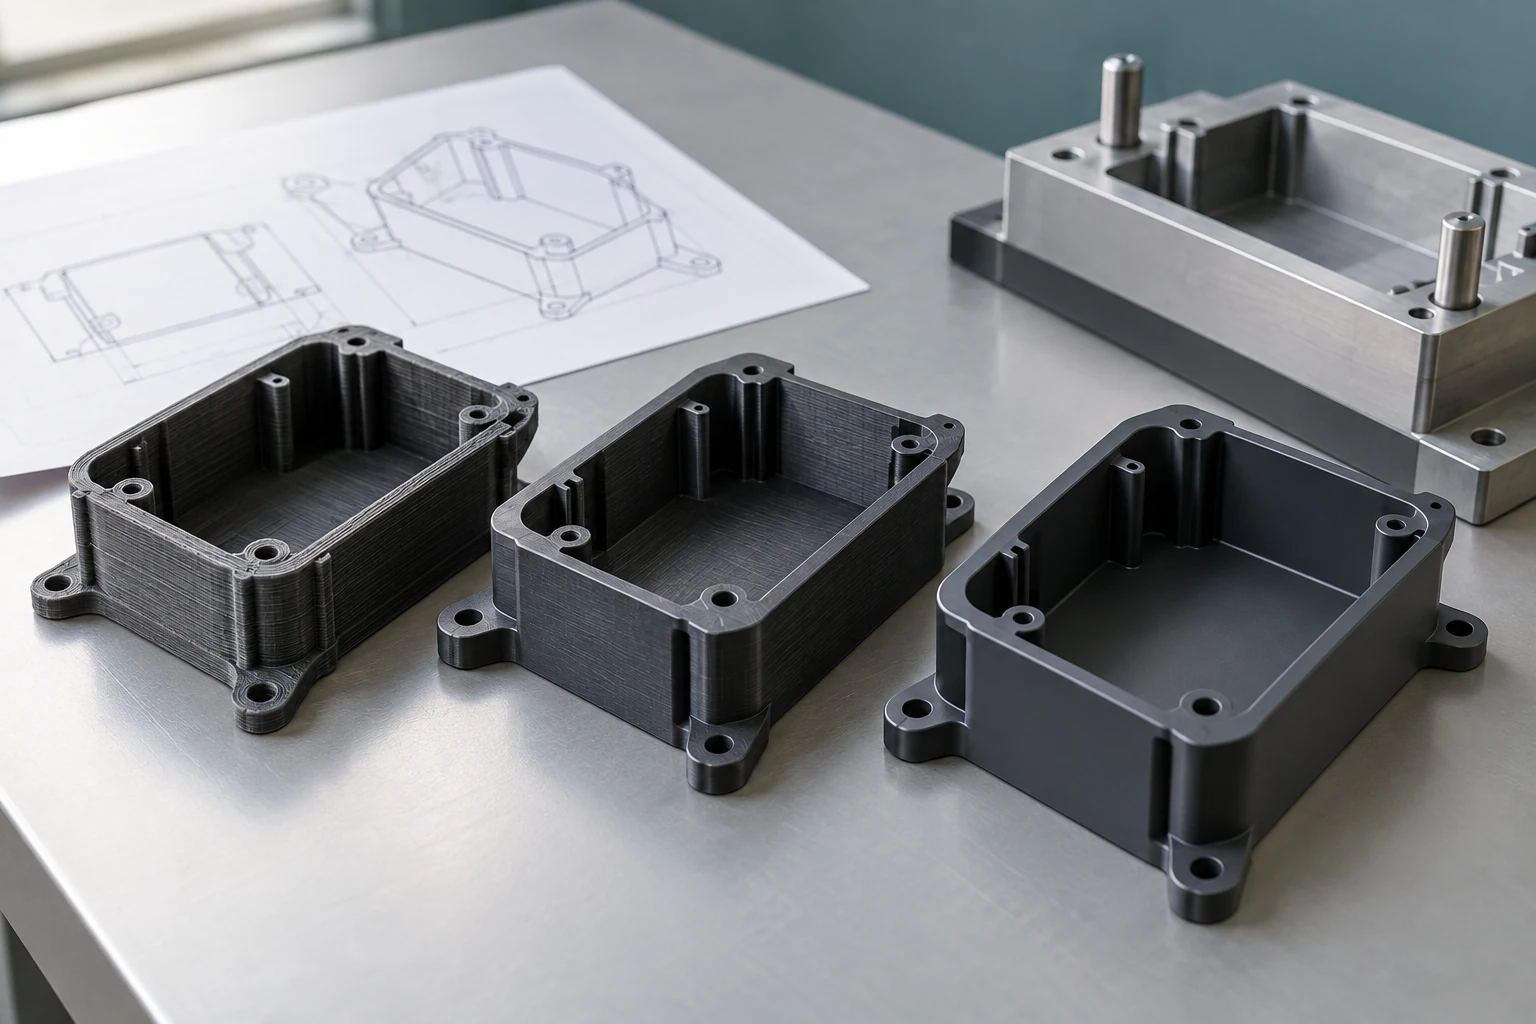
Record the purpose and test result of the current sample before choosing the next manufacturing route. A working sample and a repeatable production part answer different questions:
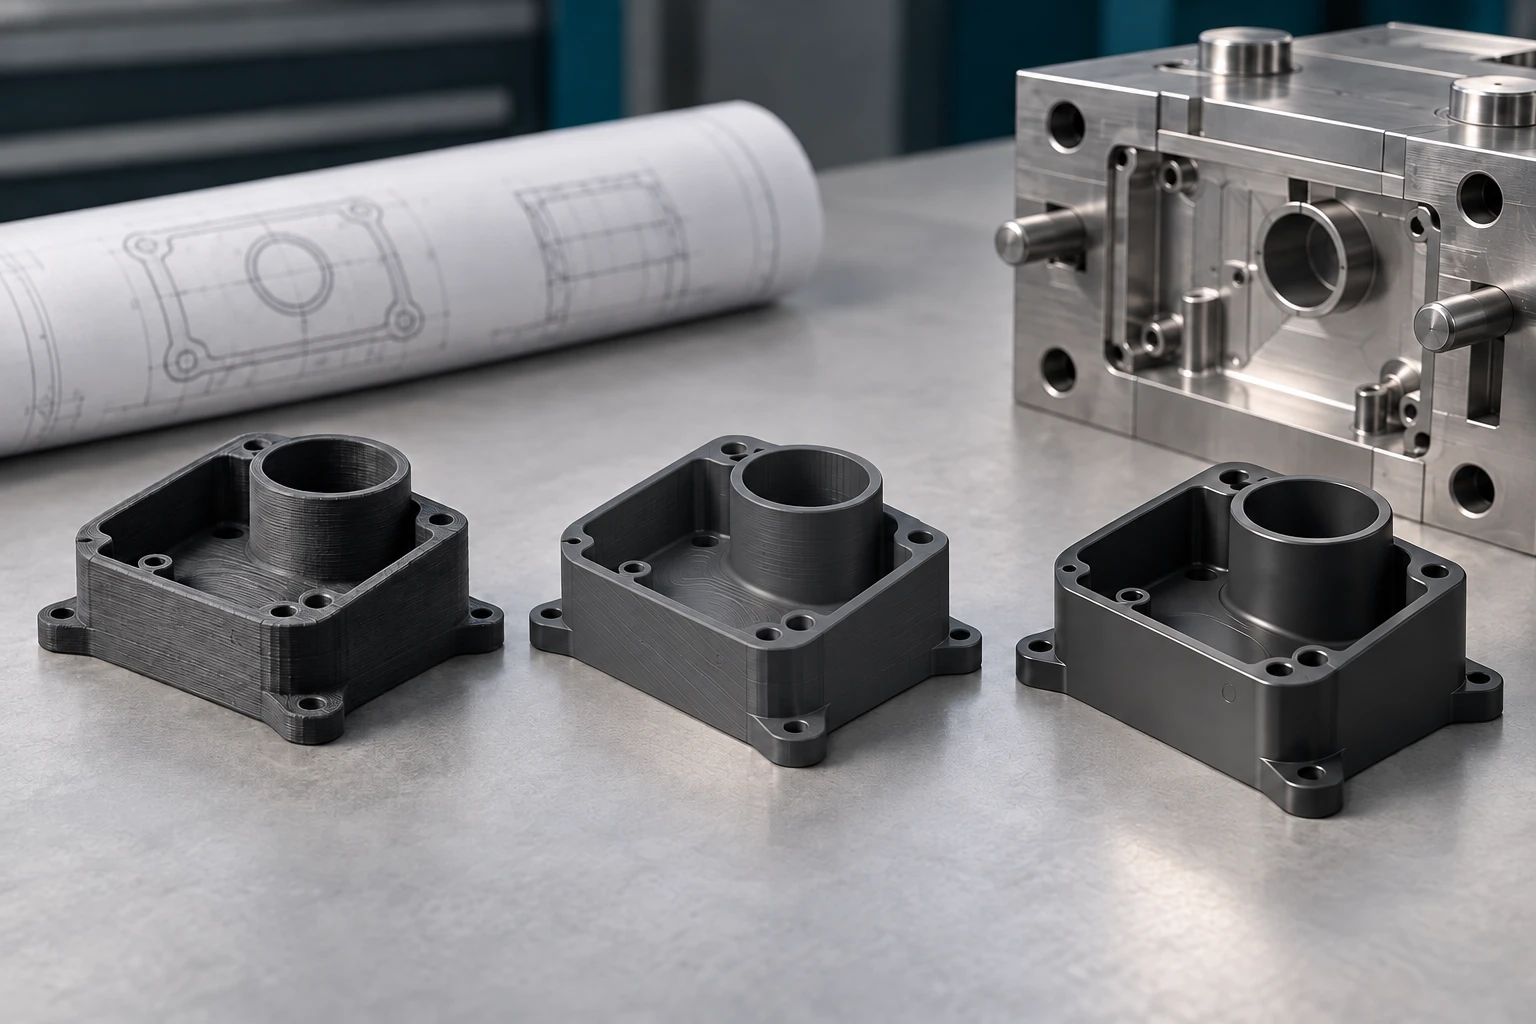
- Appearance or assembly-fit sample: a 3D-printed part can reveal shape, clearances and visual changes. It does not establish final-grade strength, molded surface quality or repeatable dimensions.
- Functional prototype: a CNC-machined or suitable printed plastic part can test a defined load, fit or mechanism. Record its material and test conditions so differences from the intended molding grade remain visible.
- Molded trial sample: a part made with the intended grade and tool can be checked against the controlled drawing. Agree the critical dimensions, function, appearance and acceptance method before repeat production.
If the sample material or process changes, repeat the tests that matter for the final application rather than treating the earlier result as production approval.
Choose the Next Manufacturing Route
There is no universal order-volume cutoff that selects a process for every plastic part. Compare the sample’s purpose with the drawing, resin, geometry, tolerances, finish and planned quantities:
- 3D printing: evaluate when the next question is visual form, assembly fit or an iteration that does not require production-tool evidence. State what the print material can and cannot validate.
- CNC plastic machining: evaluate when a functional sample or lower-quantity part needs a selected stock material and defined inspection. Confirm the stock grade, accessible features and critical dimensions.
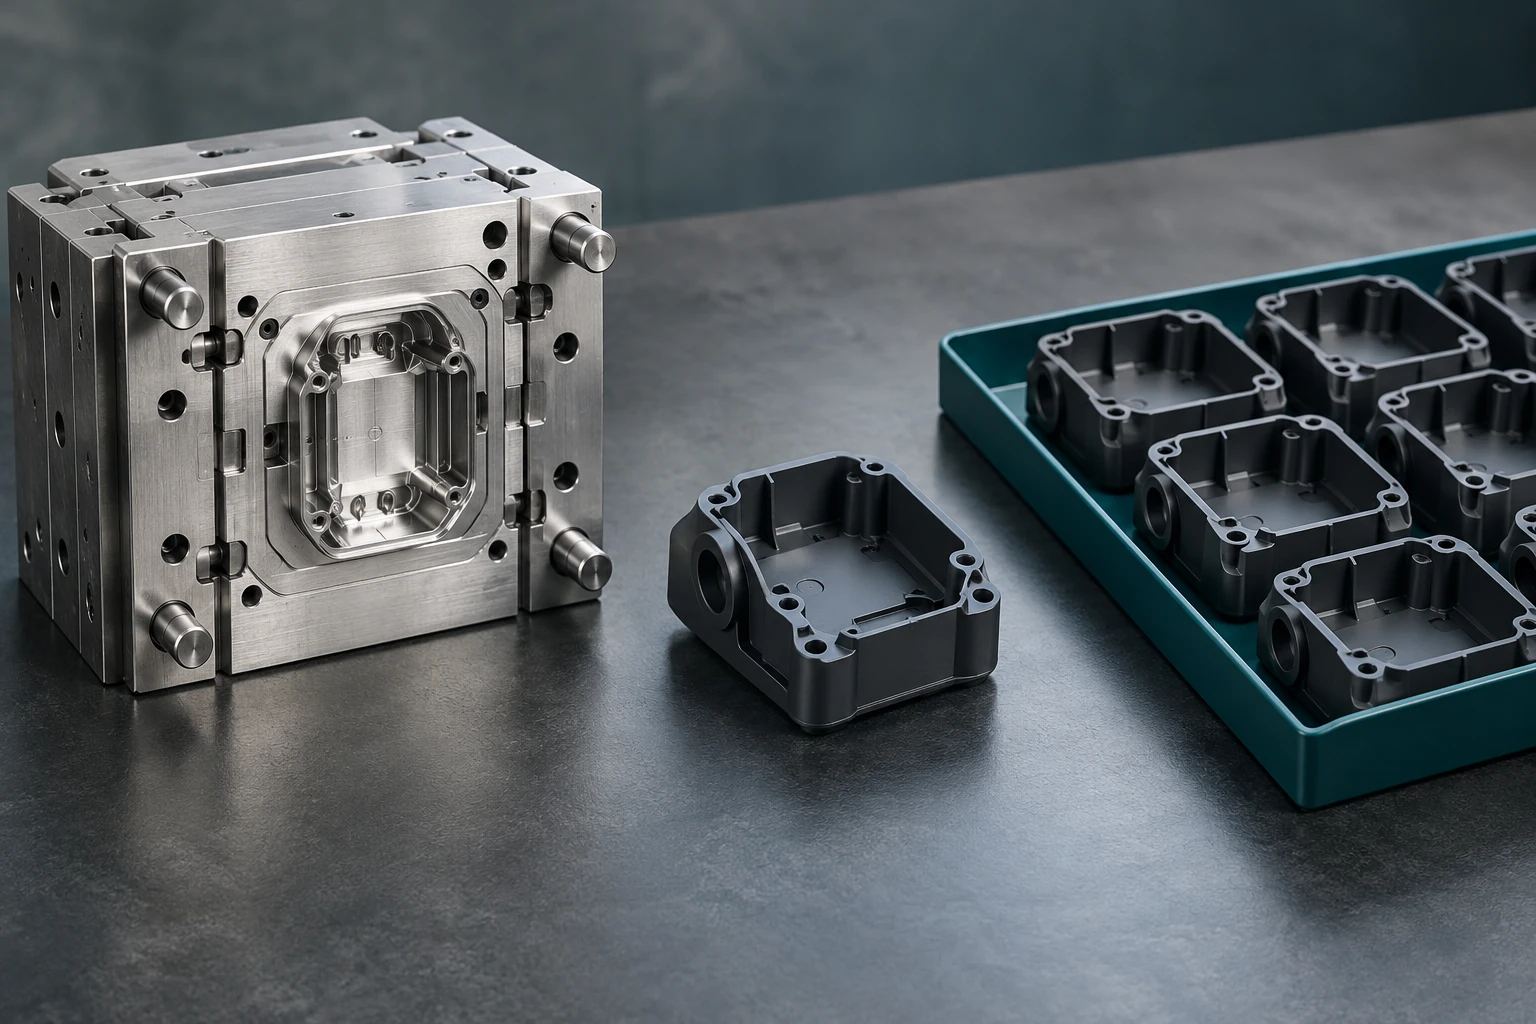
- Injection molding: evaluate when repeat molded parts and their geometry justify tooling. Review the production grade, draft, wall and rib design, gate and ejection, trial samples and release criteria before treating a prototype as a production specification.
A project may stay with machining or use different routes at different stages. For a connected material, prototype, tooling and production scope, see our integrated plastic manufacturing service. The detailed handoff checklist below lists what to include in a tooling or part RFQ.
Design for Manufacturing (DFM)
Designs that work for prototyping may not be optimal for production. Key considerations:
Material Selection
Prototype materials may differ from production materials. Consider:
- Material availability in production processes
- Cost differences between prototype and production materials
- Property differences that might affect function
- Regulatory requirements for final materials
Tolerances and Fits
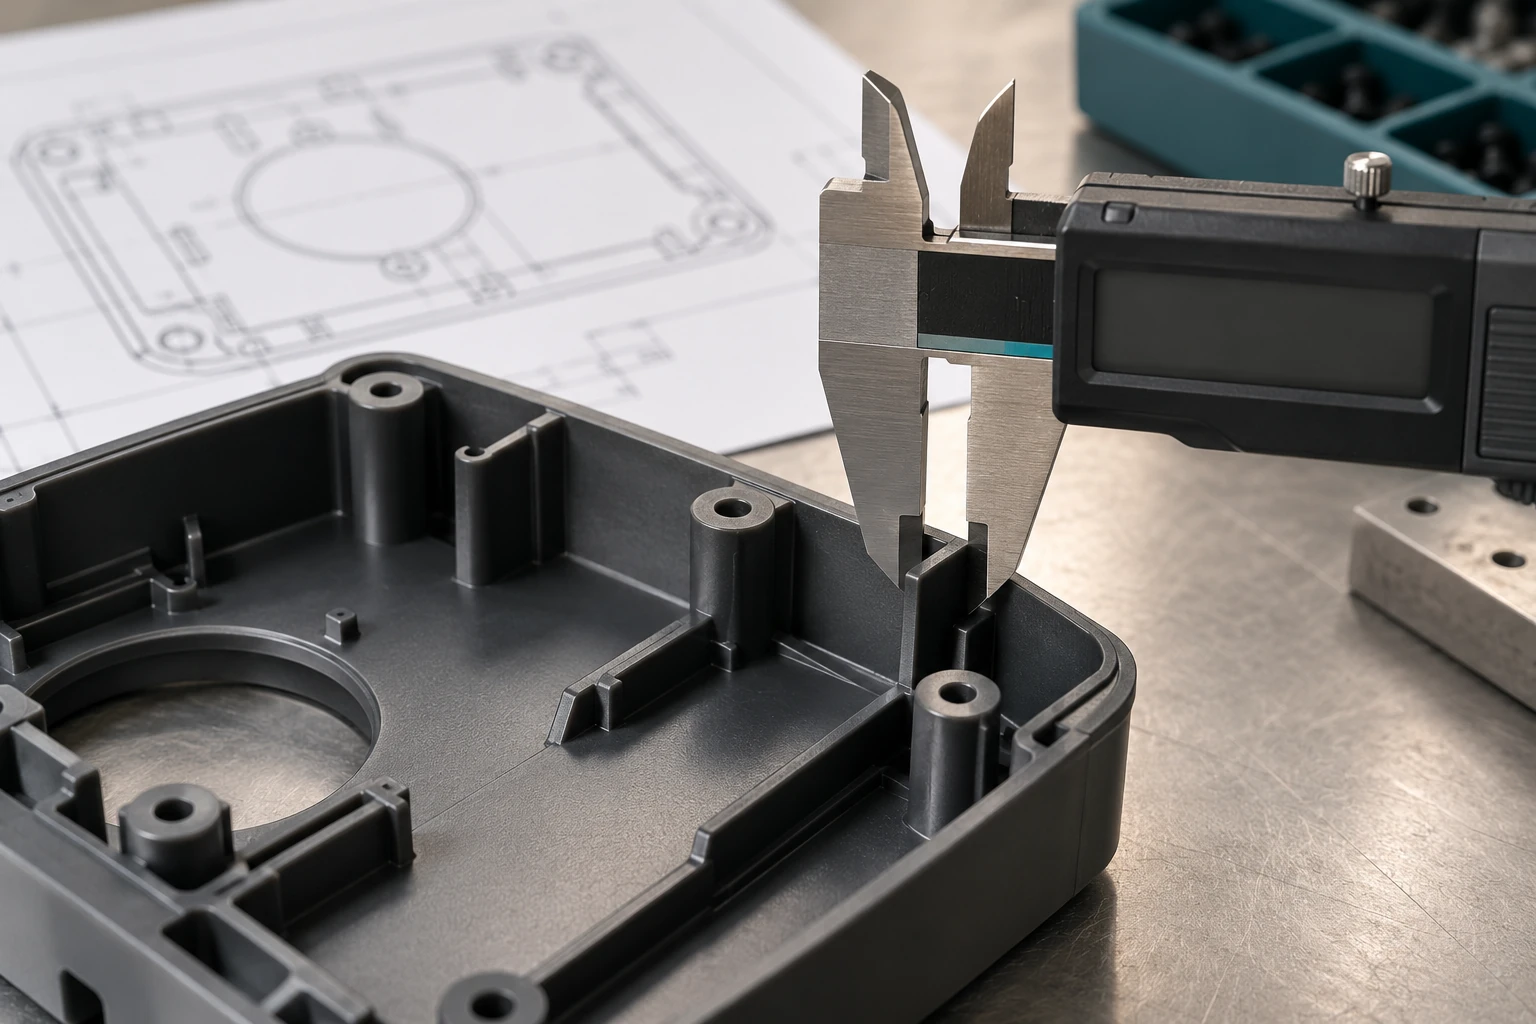
Prototype tolerances achieved through careful machining may not be economically achievable in production. Review tolerances for:
- Are tight tolerances actually necessary?
- Can assembly methods accommodate more variation?
- What’s the cost impact of specified tolerances?
Part Consolidation vs. Assembly
3D printing enables complex, consolidated parts. Production processes may favor assemblies of simpler parts. Evaluate:
- Assembly cost vs. part consolidation
- Serviceability requirements
- Quality implications of assembly vs. single parts
CNC or 3D-Printed Prototype to Injection-Molded Part: Handoff Checklist
A prototype can establish fit or function without proving how the part will mold. Use this checklist to define the production route, the evidence still needed, and the scope of a tooling or part quotation.
- Production resin and grade. Identify the intended injection-molding grade, reinforcement, color and service conditions, or state which alternatives may be reviewed. Record how the CNC or printed prototype material differs; its test result is not a specification for the molded part.
- Controlled drawing revision. Send the CAD file and dated drawing revision, critical dimensions, datums and mating-part requirements. Mark any proposed draft, wall, rib or undercut changes so prototype results are compared with the geometry actually being tooled.
- Shrinkage and measurement condition. Use the selected grade’s supplier data to plan a mold allowance, then check dimensions on molded trial samples at an agreed time and conditioning state. Part geometry, fiber orientation, gate and process settings can change the result; a single generic shrinkage figure is not a final approval.
- Gate, parting and ejection review. Agree the proposed gate and ejector locations, acceptable witness marks, appearance surfaces and any weld-line or load-bearing restrictions before the mold design is frozen.
- Trial evidence and release. Define the sample stage, critical-dimension inspection, fit or functional tests, change log and named approval responsibility. If a customer requires PPAP or another formal submission, specify that requirement separately. See the T0, T1 and T2 mold-trial checklist for a more detailed trial review.
- RFQ inputs. Include the approved drawing or CAD revision, proposed production grade, first-order and annual quantities, target timing, destination, tooling versus part scope, finish and required records. The existing request form below can be used to ask for a route and quotation review.
Technical references: the processing section of the BASF Ultramid product brochure explains why shrinkage depends on grade, geometry, gate and processing; Autodesk Moldflow gate-design guidance covers orientation, warpage and gate placement. Actual part approval remains project-specific.
Production Quality Plan
Before moving an approved sample into repeat production, specify what will be controlled, checked and recorded for your part. Include these three decisions in your RFQ:
- Production basis: confirm the drawing revision, production material and process settings that need control.
- Acceptance checks: identify critical dimensions or functions, inspection points and acceptance criteria.
- Required records: specify any material-lot, inspection or batch records needed for this order.
Cost Management at Scale
Understanding cost drivers helps optimize for production:
Fixed vs. Variable Costs
- Tooling: High fixed cost, low variable cost
- 3D Printing: Low fixed cost, high variable cost
- CNC: Medium fixed cost, medium variable cost
Economies of Scale
As volume increases, per-unit costs decrease through:
- Tooling amortization over more parts
- Setup time spread across larger batches
- Volume material discounts
- Process optimization and learning curve effects
Risk Mitigation Strategies
Scaling introduces risks. Mitigate through:
- Parallel development: Pursue multiple manufacturing approaches
- Incremental scaling: Increase volume gradually while validating quality
- Supplier qualification: Test multiple suppliers for critical components
- Inventory buffers: Maintain safety stock during transition
Our Capabilities
With over 300 CNC machines, we produce more than 10,000 pieces daily with tolerances as tight as ±0.005mm. We accept MOQ from 1 piece, with delivery times ranging from 24 hours to 15 days. Whether you need a single prototype or thousands of production parts, we have the capacity and expertise to deliver. Get a quote within 24 hours.
FAQ
Does a CNC or 3D-printed prototype prove an injection-molded part will perform the same way?
No. The prototype may verify fit or a defined function, but the stock or print material and its process can differ from the intended molding grade. Identify which tests need to be repeated on molded samples made with the production material.
When should a plastic part move from CNC machining to injection molding?
Review the drawing, material, geometry, tolerance, finish, order quantity and expected repeat demand together. Molding adds tooling and trial approval; there is no universal quantity at which it becomes the right route for every part.
What must be approved before repeat production?
Confirm the drawing revision and production grade, then agree the trial-sample checks for critical dimensions, fit, function, appearance and required records. Release criteria should match the part and the quoted scope.
What should I send for a prototype-to-production part review?
Send the CAD file or drawing revision, the current prototype and what it has proven, the application and service conditions, intended material or permitted alternatives, first-order and annual quantities, critical dimensions, finish, inspection needs, destination and target timing.
Need a route and quotation review? Use the existing form below to share your drawing and prototype context. Nylon Plastic can identify open material, tooling and sample-approval questions before confirming the quoted scope for your part.