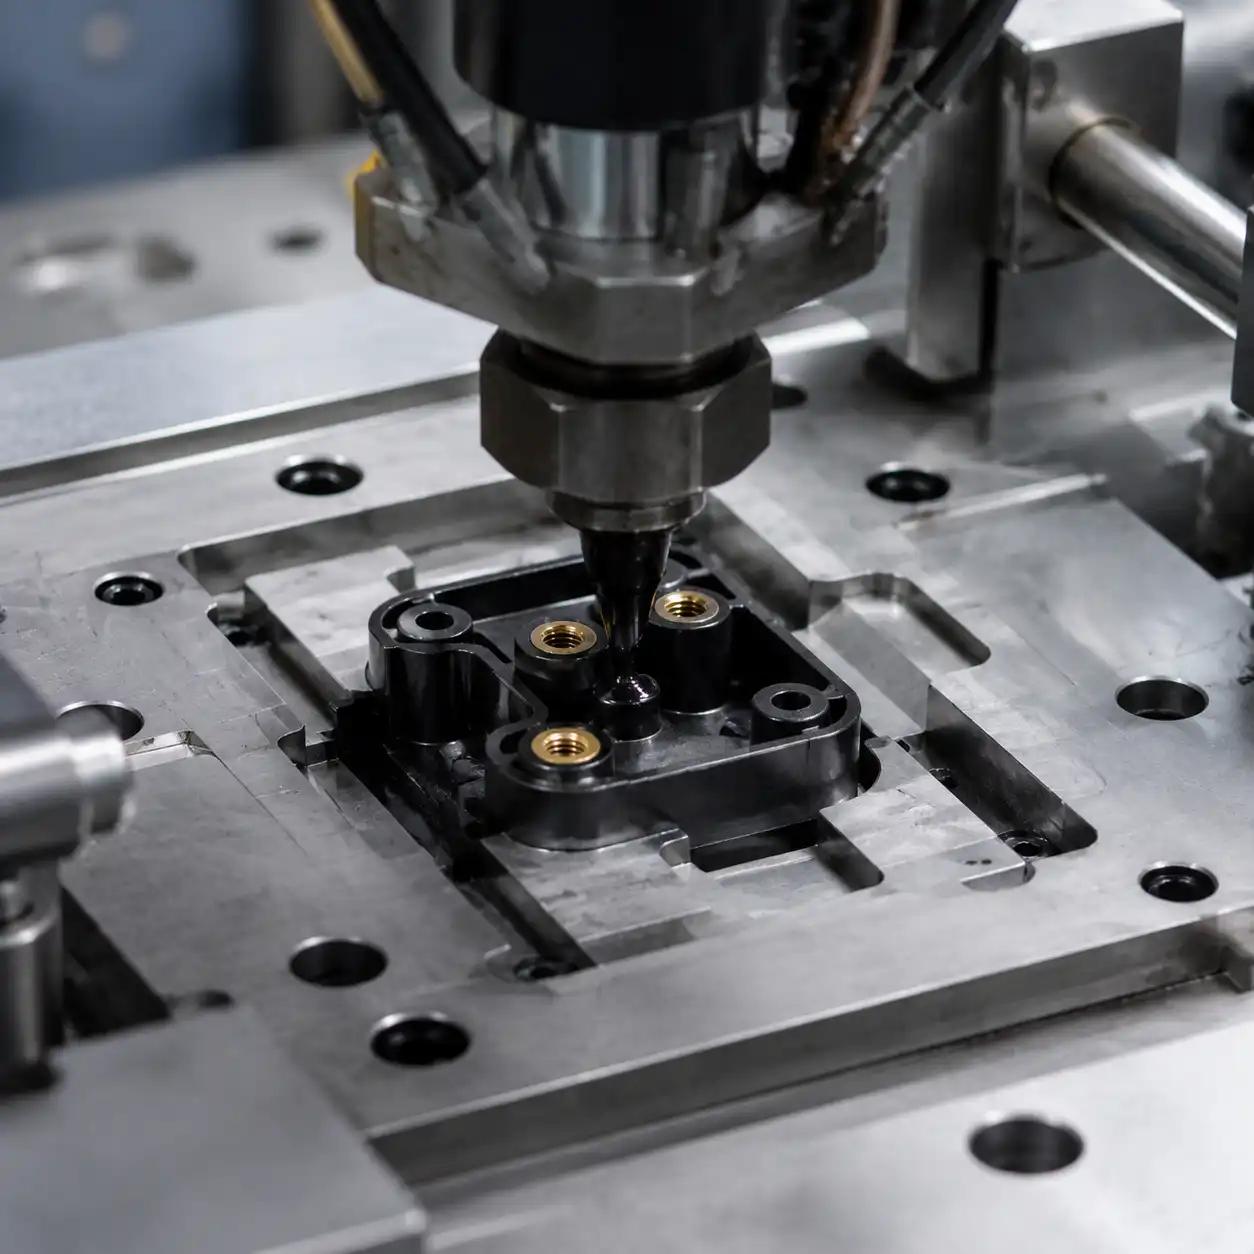
Insert molding places a prepared metal, plastic, ceramic or electrical component in the mold before molten polymer is injected around it. The process can integrate threads, contacts, pins, bushings or other functions into one molded part when the insert, resin, tooling and validation plan are designed together.
It is a practical choice when the project needs a permanent insert and repeatable location in production. It still requires an engineering review: insert movement, flash, polymer shrinkage, cracking, electrical isolation or retention failure can appear if the interface is treated as a standard molded feature.
Have a Part With Metal Inserts?
Send the part and insert drawings, polymer requirement, quantity and interface acceptance criteria. Nylon Plastic can review how resin selection, insert sourcing, positioning, tooling and molding fit together before quotation. Thread protection, torque, pull-out, sealing or electrical tests should be defined around the actual part.
When Insert Molding Fits the Project
How the Insert Molding Process Works
- Define the insert: lock the insert drawing, material, finish, thread or contact protection, cleanliness and incoming inspection requirements.
- Locate it in the tool: use a fixture, pin, shutoff or other retention feature that controls movement and orientation during mold closing and filling.
- Mold the polymer: inject the selected grade around the insert with a gate, venting and process window designed for the interface.
- Eject and inspect: check insert position, polymer coverage, flash, cracks and the dimensions agreed on the drawing.
- Validate the function: run the applicable torque, pull-out, leak, electrical, thermal or assembly test before production release.
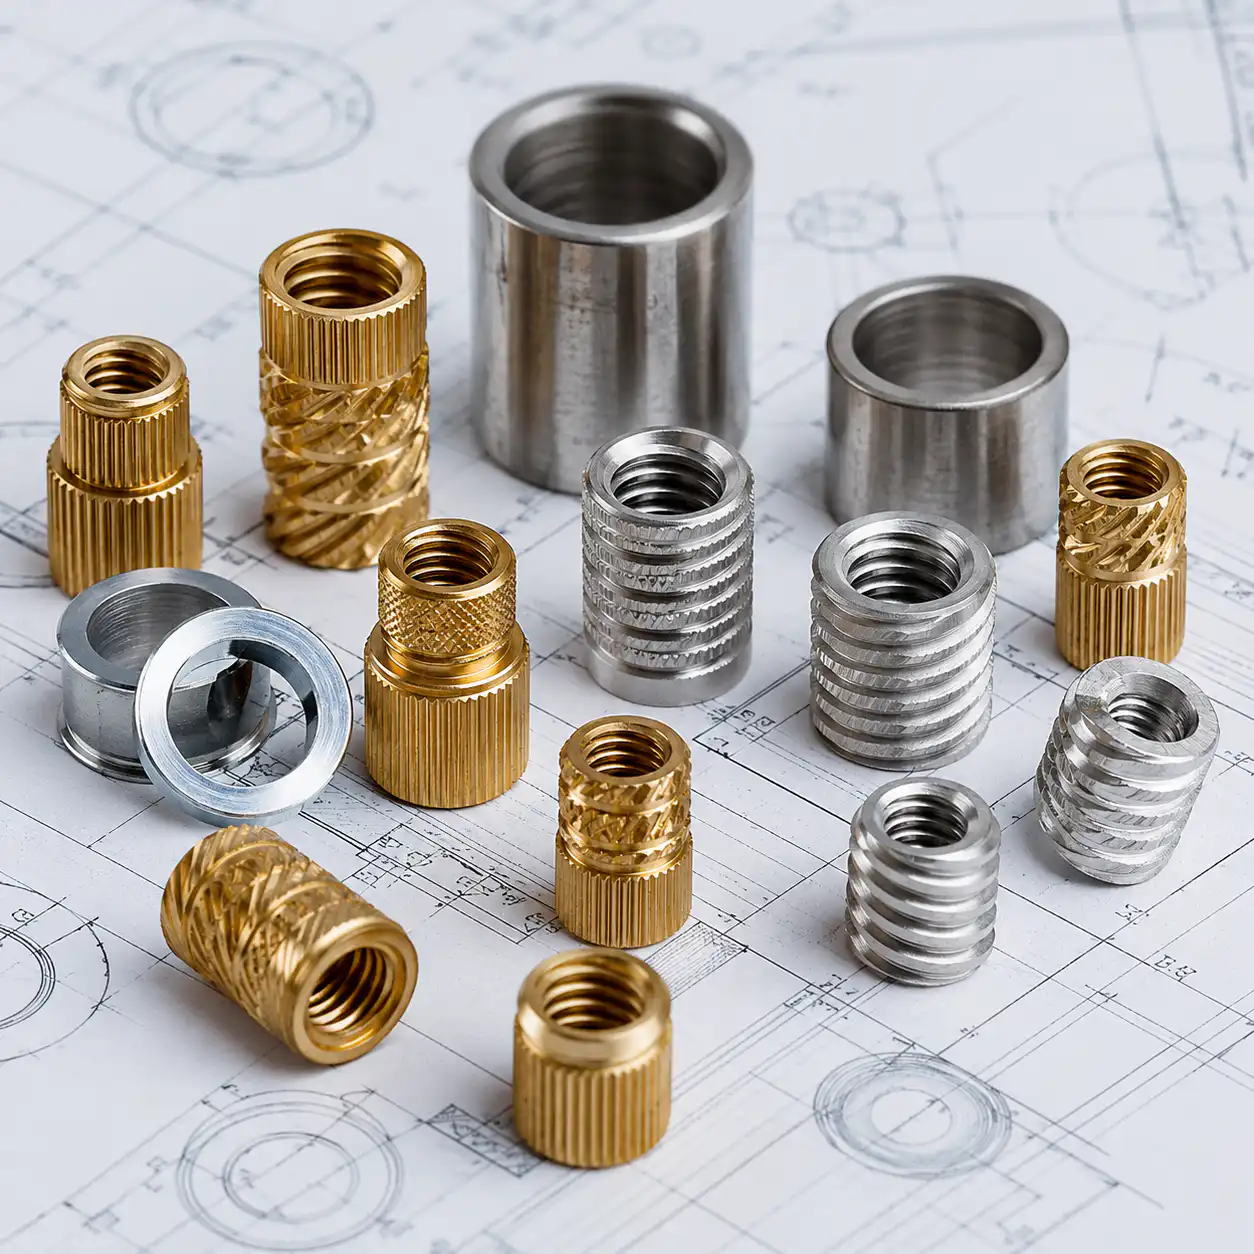
Insert and Polymer Selection
The insert and plastic cannot be selected separately. Molding temperature, polymer shrinkage, moisture response, chemical exposure, corrosion, plating, geometry and service load all affect the interface. Use the exact insert and resin specifications for approval rather than a generic material pairing.
| Item | Selection Questions | Evidence for Approval |
|---|---|---|
| Threaded insert | Thread type, blind or through hole, anti-rotation geometry, corrosion and protected faces | Insert drawing, material or plating specification, thread gauge plan, torque and pull-out requirement |
| Contact or terminal | Conductivity, plating, orientation, polymer coverage, isolation and sealing | Contact drawing, electrical test, section review and continuity or insulation criteria |
| Bushing, pin or sleeve | Alignment, wear surface, exposed length, fit and load direction | Assembly drawing, positional tolerance, load test and inspection method |
| Engineering plastic | Exact grade, reinforcement, molding window, shrinkage, moisture and service environment | Current grade data, conditioning definition, molded samples and finished-part validation |
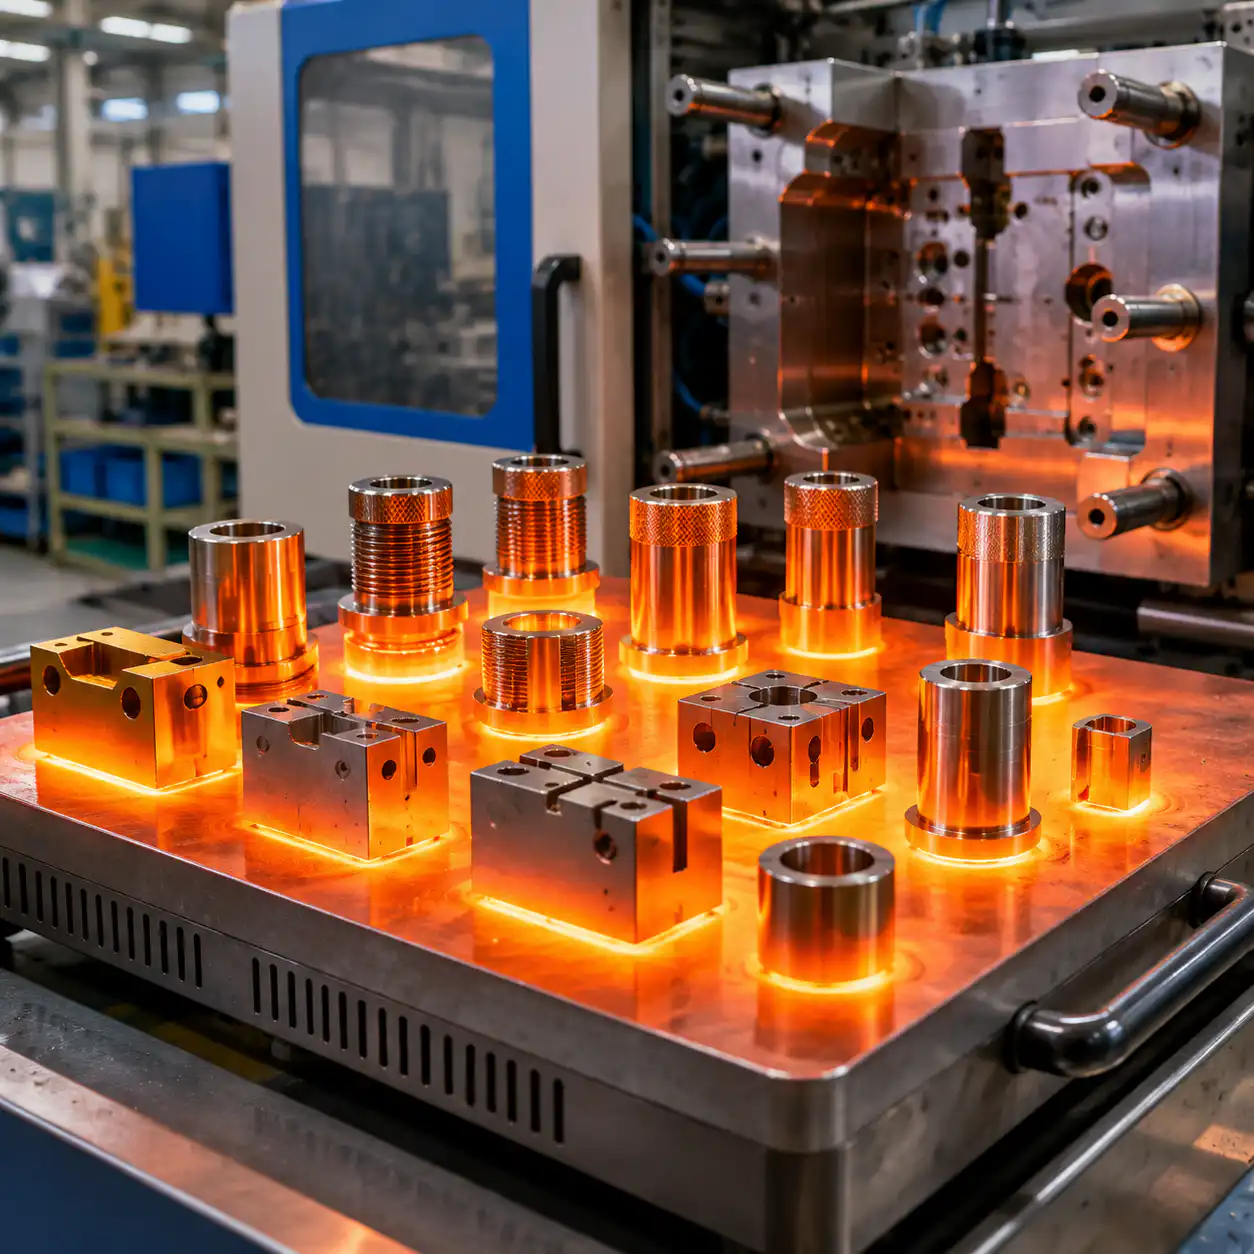
Insert Preparation and Position Control
Before molding, inserts should be checked for dimensions, contamination, burrs, plating condition and damage. Cleaning, drying or preheating may be useful for a specific material system, but those steps must follow the insert, resin and process requirements; they are not universal settings.
- Manual loading: can suit prototypes, pilot builds or parts where an operator must verify orientation before each cycle.
- Automated loading: can improve repeatability at production volume when the insert can be fed, detected and placed reliably.
- Error prevention: sensors, asymmetric fixtures, presence checks and cavity records help prevent missing or reversed inserts.
- Traceability: record insert lot, resin lot, cavity and inspection result when the interface is a critical feature.
Insert Molding Design and Tooling Review
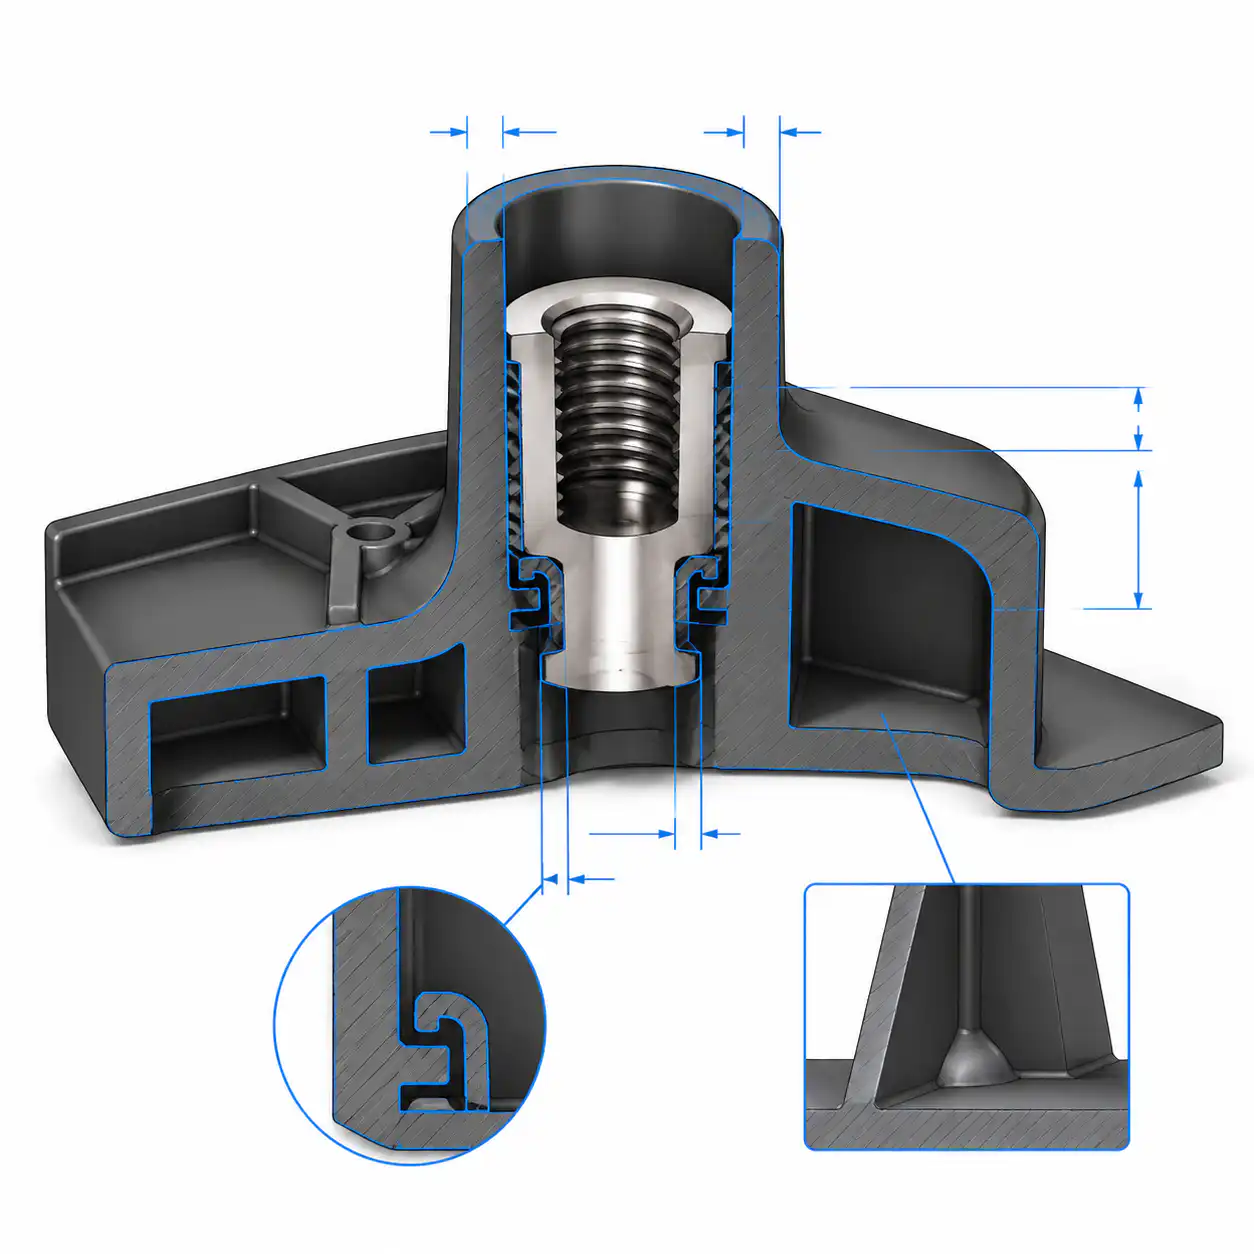
| DFM Area | What to Review | Risk if Missed |
|---|---|---|
| Retention geometry | Knurls, grooves, shoulders or other mechanical features sized for the actual load | Rotation, pull-out or local polymer damage |
| Plastic around the insert | Wall, boss, radius and transition geometry for the selected resin and shrinkage | Cracking, sink, voids or excessive residual stress |
| Gate and flow | Melt direction, weld lines, pressure on the insert and balanced filling around it | Insert shift, incomplete coverage or weak interface zones |
| Shutoff and protection | Thread, contact and sealing surfaces that must stay free of polymer or flash | Blocked threads, poor electrical contact or leak paths |
| Cooling and ejection | Part restraint, insert heat transfer, ejection force and cavity-to-cavity behavior | Warpage, marking, damage or inconsistent position |
Common Defects and Production Validation
| Observed Issue | Likely Review Area | Validation Action |
|---|---|---|
| Insert moves, tilts or is missing | Fixture, loading method, melt impingement and presence detection | Measure position by cavity and verify the loading control during the trial |
| Flash enters a thread or contact area | Insert tolerance, shutoff, protection pin and mold wear | Gauge the protected feature and inspect shutoff condition |
| Crack, gap or sink develops around the insert | Wall geometry, resin shrinkage, moisture, packing and conditioning | Section trial parts and compare dry and conditioned results where relevant |
| Torque or pull-out result is low | Retention geometry, polymer coverage, insert surface and test setup | Test production-equivalent samples against the drawing requirement |
| Electrical or sealing test fails | Coverage, contamination, flash, voids and interface path | Use the specified continuity, insulation, leak or environmental test |
Insert Molding vs Overmolding or Post-Installed Inserts
| Route | Typical Use | Main Decision |
|---|---|---|
| Insert molding | Mold plastic around a pre-positioned metal, plastic, ceramic or electrical item | Choose when permanent integration and controlled location justify dedicated tooling and interface validation |
| Overmolding | Add another polymer layer or feature over a molded or prepared substrate | Choose when grip, sealing, protection, appearance or multi-material behavior drives the design |
| Post-installed insert | Install hardware after molding by heat, ultrasonic, press or mechanical methods | Choose when serviceability, lower tooling complexity or a different assembly sequence is more important |
Applications and Procurement Fit
| Project task | What the insert contributes | What approval must define |
|---|---|---|
| Threaded mount or housing | A fastening interface integrated into the plastic | Thread, protected faces, location, installation torque and pull-out requirement |
| Electrical connector or contact carrier | A located conductive feature inside the polymer | Contact plating, exposed areas, insulation, continuity and applicable tests |
| Bushing or alignment sleeve | A wear, fit or positional interface | Concentricity, exposure, assembly fit and service loads |
| Integrated bracket or component | Combines insert and polymer functions in one part | Whole-part load path, retention, appearance and environmental validation |
Insert molding is commonly reviewed for electrical connectors and contacts, automotive and transport hardware, appliance components, industrial housings, threaded mounts and parts that combine an engineering plastic with a wear or fastening feature. The final suitability depends on the exact resin, insert specification, load and regulatory requirement.
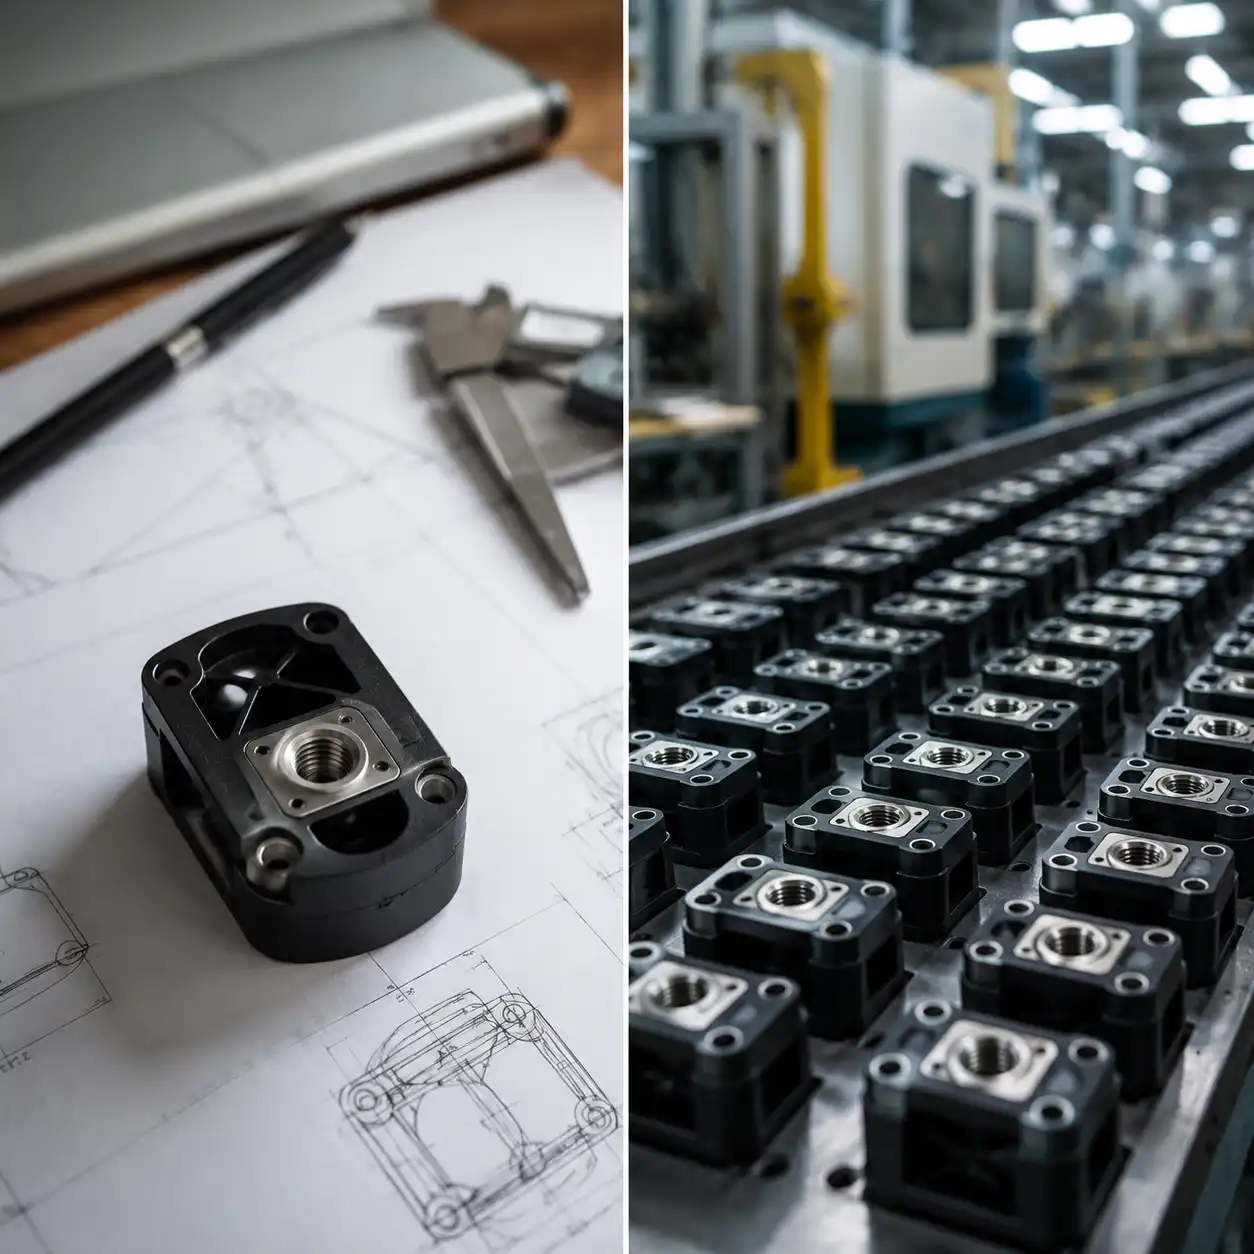
What to Send for an Insert Molding Quote
Quote the integrated part and its acceptance requirements. Confirm who supplies and approves the inserts, which faces stay free of polymer and how the interface will be tested. This avoids treating a critical insert as an unspecified purchased component.
| Quotation input | Details that change the scope |
|---|---|
| Part and insert files | CAD, controlled drawings, insert position, protected surfaces and critical dimensions |
| Insert supply | Who supplies the inserts; material, plating, thread specification, incoming inspection and lot control |
| Polymer | Mandatory grade or service conditions; reinforcement, color, conditioning and document requirements |
| Interface approval | Torque, pull-out, leak, electrical, thermal-cycle or assembly criteria and test method |
| Quantities and timing | Samples, first order, annual demand, destination and required milestones |
| Included work | Tooling, loading, molding, secondary operations, assembly, inspection, packaging and records |
Insert Molding Support From Drawing to Production
Nylon Plastic can connect engineering plastic selection, product and mold review, tooling, injection molding, inspection planning and related prototype or machining work around the project drawing. Certification and inspection documents should be confirmed for the selected material and agreed production scope.
Related Engineering Guides
- Overmolding Guide for Multi-Material Plastic Parts
- Plastic Injection Molding Services
- Metal Insert Molding for Plastic Parts
- Insert Molding vs Overmolding
Frequently Asked Questions
What is insert molding?
Insert molding positions a prepared component in the mold before plastic is injected around it, creating an integrated molded part.
How is insert molding different from overmolding?
Insert molding usually integrates a pre-made component such as a threaded insert or contact. Overmolding adds another polymer over a substrate to create grip, sealing, protection or multi-material behavior.
Can threaded metal inserts be insert molded?
Yes. The insert drawing, retention geometry, thread protection, location method, resin shrinkage and required torque or pull-out result should be reviewed together.
What is needed for an insert molding quotation?
Provide the part and insert drawings, resin requirement, functional tests, quantity, destination and target timing. Existing samples or defect records help when the project replaces a current assembly.
Does insert molding always create a chemical bond to metal?
No. Retention can depend on geometry and mechanical interlock. Do not assume adhesion or sealing from material names alone; validate the interface against the required load or leak test.
Must every insert be preheated?
No. Preparation depends on the insert, polymer and process. Any cleaning, drying or preheating step needs a defined purpose and qualified conditions for that material system.
Request an Insert Molding Review
Use the form below for an insert-molded part review. The team can identify feasibility questions and the integrated manufacturing scope to quote.