PA6 GF30 is Nylon 6 reinforced with a nominal 30% glass fiber by weight. It is selected when unfilled PA6 does not provide enough stiffness, creep resistance or dimensional stability. This guide combines a real commercial-grade datasheet, typical cross-supplier property ranges, moisture effects and injection-molding starting conditions.
PA6 GF30 at a Glance
Use the values below for initial material screening. Final design values must come from the selected grade datasheet, the stated conditioning method and molded-part validation.
What Does PA6 GF30 Mean?
- PA6 identifies Polyamide 6, also called Nylon 6.
- GF identifies glass-fiber reinforcement.
- 30 identifies the nominal glass-fiber content by weight.
PA6 GF30 is a material family, not one universal recipe. Heat stabilizers, impact modifiers, lubricants, pigments, flame retardants, resin viscosity and fiber system can all change the final properties and molding behavior. Two materials marked PA6 GF30 are therefore not automatically interchangeable.
PA6 WHG30A Manufacturer Datasheet
The downloadable manufacturer TDS identifies the commercial grade as PA6 WHG30A. The following values are reproduced from that one-page document. They are typical product values, not guaranteed design limits.
| Property | Test Standard | Unit | PA6 WHG30A |
|---|---|---|---|
| Tensile Strength | ISO 527-2 | MPa | 165 |
| Tensile Strain at Break | ISO 527-2 | % | 9 |
| Flexural Strength | ISO 527-2 | MPa | 230 |
| Flexural Modulus | ISO 178 | MPa | 6000 |
| Izod Notched Impact Strength | ISO 179 | kJ/m2 | 17 |
| Temperature of Deflection Under Load | ISO 75-2/B | °C | 175 |
| Melting Index | ISO 1183 | g/10 min | 20 |
| Density | ISO 1183 | g/cm3 | 1.36 |
| Molding Shrinkage | ISO 2577 | % | 0.6 |
| Flammability | UL 94 | – | – |
Document note: The source document lists the test standards exactly as shown above. For a regulated or safety-critical project, request the current signed TDS, certificate of analysis and any required RoHS, REACH or UL documentation.
PA6 GF30 Typical Property Data
The following tables summarize typical ranges seen across commercial PA6 GF30 grades. They are useful for comparison and early design screening. Differences from the PA6 WHG30A table above can result from formulation, specimen thickness, test standard and conditioning state.
PA6 GF30 Mechanical Properties (Dry as Molded, 23 C)
| Property | Value (Typical Range) | Test Method | Unit |
|---|---|---|---|
| Tensile Modulus | 9,500-10,500 | ISO 527-1/-2 | MPa |
| Tensile Strength at Break | 170-190 | ISO 527-1/-2 | MPa |
| Elongation at Break | 3.0-4.5 | ISO 527-1/-2 | % |
| Flexural Modulus | 8,000-9,500 | ISO 178 | MPa |
| Flexural Strength | 260-290 | ISO 178 | MPa |
| Charpy Impact Strength (notched) | 12-16 | ISO 179/1eA | kJ/m2 |
| Charpy Impact Strength (unnotched) | 75-95 | ISO 179/1eU | kJ/m2 |
| Izod Impact Strength (notched) | 11-15 | ISO 180/A | kJ/m2 |
| Ball Indentation Hardness | 200-230 | ISO 2039-1 | MPa |
Physical Properties
| Property | Value (Typical Range) | Test Method | Unit |
|---|---|---|---|
| Density | 1.35-1.38 | ISO 1183 | g/cm3 |
| Water Absorption (23 C, saturation) | 5.5-6.5 | ISO 62 | % |
| Water Absorption (23 C, 50% RH equilibrium) | 1.5-2.0 | ISO 62 | % |
| Molding Shrinkage (parallel, 1.6 mm) | 0.25-0.40 | ISO 294-4 | % |
| Molding Shrinkage (normal, 1.6 mm) | 0.80-1.10 | ISO 294-4 | % |
| Post-Molding Shrinkage (parallel, 1h at 110 C) | 0.05-0.10 | ISO 294-4 | % |
| Post-Molding Shrinkage (normal, 1h at 110 C) | 0.10-0.15 | ISO 294-4 | % |
Thermal Properties
| Property | Value (Typical Range) | Test Method | Unit |
|---|---|---|---|
| Melting Temperature (DSC, 10 K/min) | 218-222 | ISO 11357-1/-3 | C |
| HDT at 0.45 MPa | 215-220 | ISO 75-1/-2 | C |
| HDT at 1.8 MPa | 195-210 | ISO 75-1/-2 | C |
| Vicat Softening Temperature (VST/B50) | 205-215 | ISO 306 | C |
| Coefficient of Linear Thermal Expansion (parallel, 23-55 C) | 2.0-3.0 x 10⁻⁵ | ISO 11359-1/-2 | 1/K |
| Coefficient of Linear Thermal Expansion (normal, 23-55 C) | 6.0-9.0 x 10⁻⁵ | ISO 11359-1/-2 | 1/K |
| Thermal Conductivity | 0.28-0.35 | DIN 52612 | W/(m·K) |
| Specific Heat Capacity | 1.5-1.7 | — | J/(g·K) |
Electrical Properties
| Property | Value (Typical Range) | Test Method | Unit |
|---|---|---|---|
| Dielectric Constant (1 MHz) | 3.5-4.5 | IEC 60250 | — |
| Dissipation Factor (1 MHz) | 0.01-0.03 | IEC 60250 | — |
| Volume Resistivity | 1013-1015 | IEC 60093 | ohm·cm |
| Surface Resistivity | 1012-1014 | IEC 60093 | ohm |
| Comparative Tracking Index (CTI) | 500-600 | IEC 60112 | V |
| Dielectric Strength (1.6 mm) | 30-35 | IEC 60243-1 | kV/mm |
Flammability
| Property | Value | Test Method | Notes |
|---|---|---|---|
| UL 94 Rating (0.8 mm) | HB | UL 94 | Standard GF30 is not flame retardant |
| UL 94 Rating (1.6 mm) | HB | UL 94 | FR V-0 requires specialized FR compound |
| Limiting Oxygen Index (LOI) | 22-24% | ISO 4589 | Burns in normal atmosphere |
| Auto-Ignition Temperature | >400 C | ASTM D1929 | — |
Property Changes with Moisture Conditioning
PA6 absorbs moisture from the environment. At equilibrium with 50% RH at 23 C, a PA6 GF30 part will absorb approximately 1.5-2.0% water by weight. This changes the mechanical properties significantly. Tensile strength decreases by 30-40%, flexural modulus by 25-35%, and impact strength increases by 50-100%. The data table below shows the approximate shift from dry-as-molded to conditioned (50% RH) values:
| Property | Dry (as molded) | Conditioned (50% RH, 23 C) | Change |
|---|---|---|---|
| Tensile Strength (MPa) | 180 | 110-130 | -30 to -40% |
| Flexural Modulus (GPa) | 9.0 | 6.0-7.0 | -25 to -35% |
| Charpy Notched Impact (kJ/m2) | 14 | 20-28 | +50 to +100% |
| HDT at 1.8 MPa (C) | 200 | 65-75 (wet) | Significant drop at full saturation |

Processing Parameters
Drying
PA6 GF30 must be dried to a moisture content below 0.10% (target 0.05%) before injection molding. Recommended drying: 80 C for 4-6 hours in a desiccant dryer with a dew point of -30 C or lower. Tray drying at 80 C for 8-12 hours is acceptable for non-critical applications but is less reliable than desiccant drying. Do not dry above 90 C — oxidative discoloration (yellowing) begins at higher temperatures.
Injection Molding
| Parameter | Recommended Range | Notes |
|---|---|---|
| Melt Temperature (nozzle) | 250-280 C | Lower end for thin walls, upper for thick |
| Mold Temperature | 80-100 C | 100 C preferred for crystallinity and surface |
| Injection Speed | Medium to fast | Faster fill reduces fiber orientation variation |
| Hold Pressure | 50-80% of injection pressure | Enough to pack out shrinkage, avoid overpacking |
| Back Pressure | 5-15 bar (hydraulic) | Higher back pressure improves melt homogeneity |
| Screw Speed | 50-150 rpm | Lower end for larger shot sizes to avoid shear heating |
| Residence Time (max at melt temp) | 10-15 minutes | Purge if longer; degraded PA6 produces burn marks and strength loss |
Mold Design Considerations
- Gate type: All standard gate types are suitable. Pin gates, edge gates, and fan gates all work. Tunnel (submarine) gates require attention to gate diameter — minimum 0.8 mm to avoid excessive shear with 30% GF.
- Gate location: Position the gate so flow is into the thickest section. Avoid long flow paths that allow the melt front to cool before the cavity fills.
- Venting: Adequate venting is critical. Poor venting leads to burn marks, short shots, and die buildup. Vent depth: 0.01-0.02 mm.
- Draft angle: Minimum 1 degree, 2 degrees preferred for textured surfaces. GF grades shrink tightly onto cores — adequate draft prevents ejection damage.
- Steel selection: 30% glass fiber is abrasive. For production runs exceeding 100,000 shots, use hardened tool steel (min. 52 HRC) for cavities and cores, especially at gates and high-wear areas.
Comparing PA6 GF30 with Related Grades
PA6 GF30 is the most common glass-filled nylon, but it is not always the best choice. Here is how it compares numerically with neighboring grades:
| Property | PA6 Unfilled | PA6 GF15 | PA6 GF30 | PA6 GF50 | PA66 GF30 |
|---|---|---|---|---|---|
| Tensile Strength (MPa) | 80 | 120-140 | 170-190 | 200-230 | 180-200 |
| Flexural Modulus (GPa) | 2.8 | 5.5-6.5 | 8.0-9.5 | 14-16 | 9.0-10.5 |
| Notched Izod (kJ/m2) | 5-7 | 7-10 | 11-15 | 13-18 | 10-13 |
| HDT at 1.8 MPa (C) | 65-75 | 180-195 | 195-210 | 210-215 | 240-255 |
| Density (g/cm3) | 1.14 | 1.23 | 1.36 | 1.56 | 1.37 |
| Relative Cost | 1.0x | 1.1x | 1.2x | 1.4x | 1.3x |
PA6 Glass Fiber Grade Comparison: GF15 vs GF30 vs GF40 vs GF50
Glass fiber content drives the performance-cost trade-off in PA6 compounds. The table below shows how increasing glass fiber from 15% to 50% changes key mechanical and thermal properties. Use these screening values to narrow your grade selection before requesting commercial datasheets.
| Property | PA6 Unfilled | PA6 GF15 | PA6 GF30 | PA6 GF40 | PA6 GF50 |
|---|---|---|---|---|---|
| Tensile Strength (MPa, dry) | 70 – 85 | 110 – 130 | 160 – 190 | 180 – 200 | 200 – 220 |
| Flexural Modulus (MPa) | 2,500 – 3,000 | 4,500 – 5,500 | 8,000 – 10,000 | 10,500 – 12,000 | 13,000 – 15,000 |
| Elongation at Break (%) | 20 – 40 | 3 – 5 | 3 – 5 | 2 – 3 | 1.5 – 2.5 |
| Charpy Notched Impact (kJ/m², 23°C) | 5 – 8 | 8 – 12 | 10 – 15 | 12 – 16 | 13 – 17 |
| Density (g/cm³) | 1.13 – 1.15 | 1.20 – 1.23 | 1.35 – 1.38 | 1.44 – 1.48 | 1.55 – 1.58 |
| HDT/A, 1.8 MPa (°C) | 60 – 75 | 180 – 195 | 200 – 210 | 210 – 215 | 215 – 220 |
| Melting Point (°C) | 220 – 225 | 220 – 225 | 220 – 225 | 220 – 225 | 220 – 225 |
| Mold Shrinkage (flow, %) | 1.0 – 1.5 | 0.4 – 0.7 | 0.2 – 0.5 | 0.15 – 0.35 | 0.10 – 0.25 |
| Typical Applications | Non-structural clips, covers | Housings, brackets, medium stiffness | Engine covers, fan shrouds, power tool housings | High-stiffness frames, pump bodies | Metal replacement, extreme rigidity |
Selection guidance: PA6 GF30 is the most commonly specified glass-filled PA6 grade because it delivers the best stiffness-to-cost ratio for typical structural applications. Move to GF40 or GF50 only when the application demands stiffness approaching aluminum or when wall thickness is constrained. Stay with GF15 when flow into thin-wall features or impact toughness at low temperature matters more than maximum rigidity.
PA6 GF30 Commercial Grade Equivalents
| Supplier | PA6 GF30 Grade | Key Features |
|---|---|---|
| BASF | Ultramid B3WG6 / B3EG6 | General-purpose, heat-stabilized, excellent surface finish |
| DuPont | Zytel 73G30 HSL | Heat-stabilized, widely specified in automotive |
| LANXESS | Durethan BKV 30 H2.0 | Heat-aged, good flow for thin-wall parts |
| DSM / Envalior | Akulon K224-G6 | General-purpose, good chemical resistance |
| Domo / Solvay | Technyl C216 V30 | Widely available in Asia, good processability |
| EMS-Grivory | Grilon BG-30 | Good impact balance, suitable for structural parts |
| Radici | Radilon S RV300 | Easy flow, suitable for complex geometries |
| Ensinger | TECAMID 6 GF30 | Stock shapes and machined parts |
When substituting between PA6 GF30 suppliers, compare full datasheets in the same conditioned state (dry-as-molded vs 50% RH), verify mold shrinkage in both flow and transverse directions, and run a production-tool trial. Even nominally equivalent PA6 GF30 grades differ in fiber length retention, color stability, heat aging, and processing window.
Where PA6 GF30 Is Used
PA6 GF30 is commonly considered for structural parts that need higher stiffness and heat resistance than unfilled PA6. The selected commercial grade still has to meet the part’s impact, moisture, chemical, appearance, electrical and flame requirements.
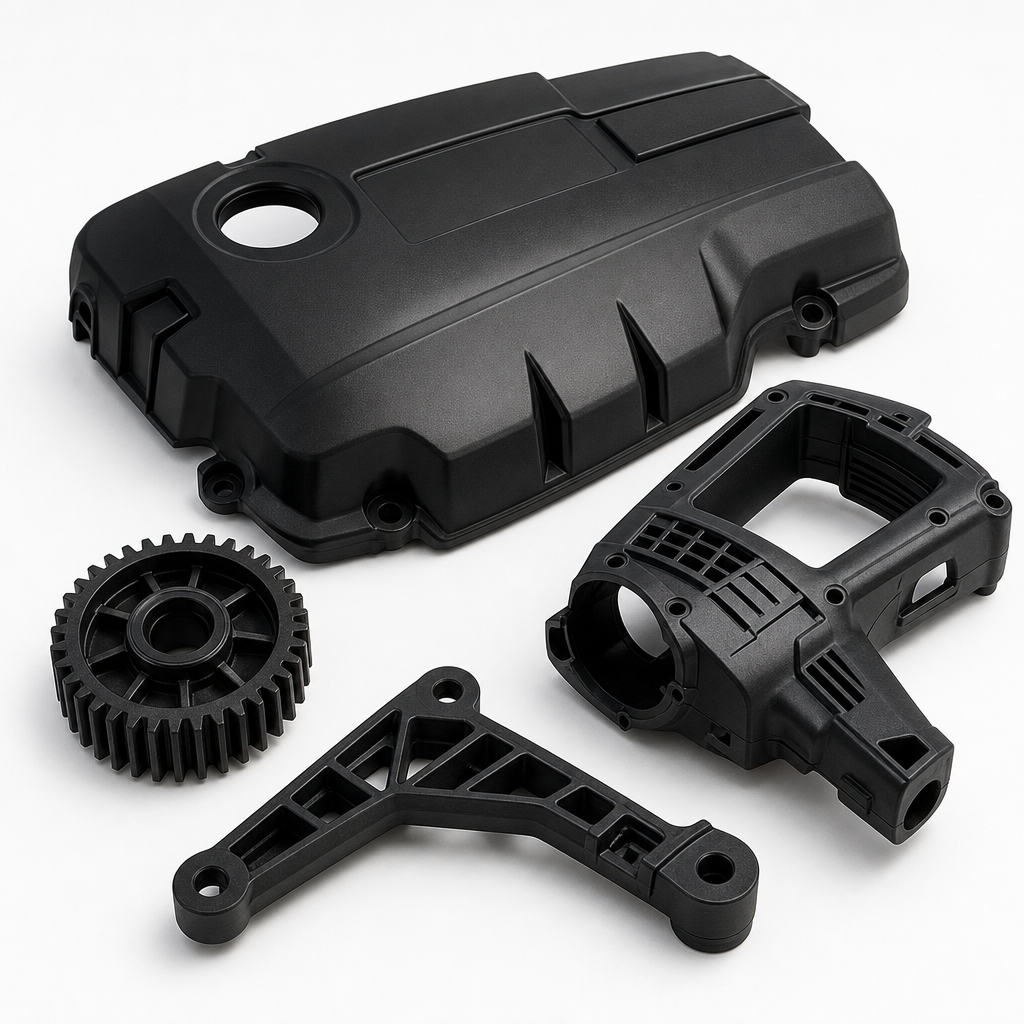
Fan shrouds, structural housings, brackets and selected under-hood components.
Pump bodies, impellers, machine housings and load-bearing supports.
Housings, connectors and supports when the grade meets the required electrical and flammability ratings.
Stiff housings, frames and mechanical components where fiber orientation and surface finish are controlled.
About Our Engineering Plastics Supply
As an ISO 9001 certified engineering plastics manufacturer and exporter, we produce PA6 GF30 in heat-stabilized, impact-modified, UV-stabilized, and color-matched variants. Our standard grade carries UL 94 HB certification with full RoHS and REACH compliance. We supply B2B buyers worldwide with batch-specific certificates of analysis and application engineering support. For your specific requirements — whether you need a standard datasheet grade or a custom formulation — contact our technical team with your target properties and annual volume.
Need a PA6 GF30 datasheet for your application or a quotation for supply? Contact our team — specify your volume, delivery destination, and any special requirements (color, certification, impact modification). We respond with datasheet and pricing within one business day.
Frequently Asked Questions
Is PA6 GF30 one standardized material?
No. PA6 GF30 identifies a PA6 material family with a nominal 30% glass-fiber level. The additive package, resin viscosity, fiber system and conditioning state vary by commercial grade, so compare the complete TDS and validate the molded part.
Is PA6 GF30 the same as PA66 GF30?
No. Both contain nominal 30% glass fiber, but PA6 and PA66 use different base polymers. They differ in melting and heat performance, moisture response, processing window and grade availability.
Is standard PA6 GF30 flame retardant?
Not automatically. A standard grade and a PA6 GF30 FR grade are separate selections. Confirm the exact UL 94 rating, specimen thickness and certification for the chosen commercial grade.
What are the key properties to check in a PA6-GF30 datasheet?
Focus on tensile strength (typically 170-190 MPa), flexural modulus (7,000-9,000 MPa), notched Izod impact (10-15 kJ/m²), HDT at 1.8 MPa (195-215°C), density (1.35-1.38 g/cm³), mold shrinkage (0.2-0.5%), and melt flow rate.
Why does PA6-GF30 datasheet strength vary between suppliers?
Variations come from differences in glass fiber type (E-glass vs. others), fiber length distribution, coupling agent quality, and base resin molecular weight. A datasheet showing ±5% deviation from these ranges is within industry norms.
How should I read PA6-GF30 datasheet values for my design?
Use “conditioned” values (tested at 23°C/50% RH equilibrium) for parts operating in ambient environments, and “dry-as-molded” values for parts in dry or sealed applications. Safety factors of 1.5-2.5× should be applied to datasheet ultimate properties for design calculations.
What processing parameters does a good PA6-GF30 datasheet include?
A complete datasheet should specify melt temperature (260-280°C), mold temperature (80-100°C), drying conditions (80°C/4-6h to <0.15% moisture), injection speed (medium-high), and recommended back pressure (0.3-0.7 MPa) to prevent fiber degradation.

