Nylon chemical resistance to cleaning chemicals is usually fine for brief wipe-downs, but repeated wash cycles, hot alkaline cleaners, and oxidizing disinfectants can change the result fast. In production, cleaning is often harsher than the process fluid itself.
If you need the broader chemical view first, start with the nylon chemical compatibility chart and the nylon chemical resistance guide.
Bottom line: brief wipe-downs are usually manageable, but hot alkaline washes and oxidizing cleaners need the same seriousness you would give a process-fluid exposure test.
At a Glance
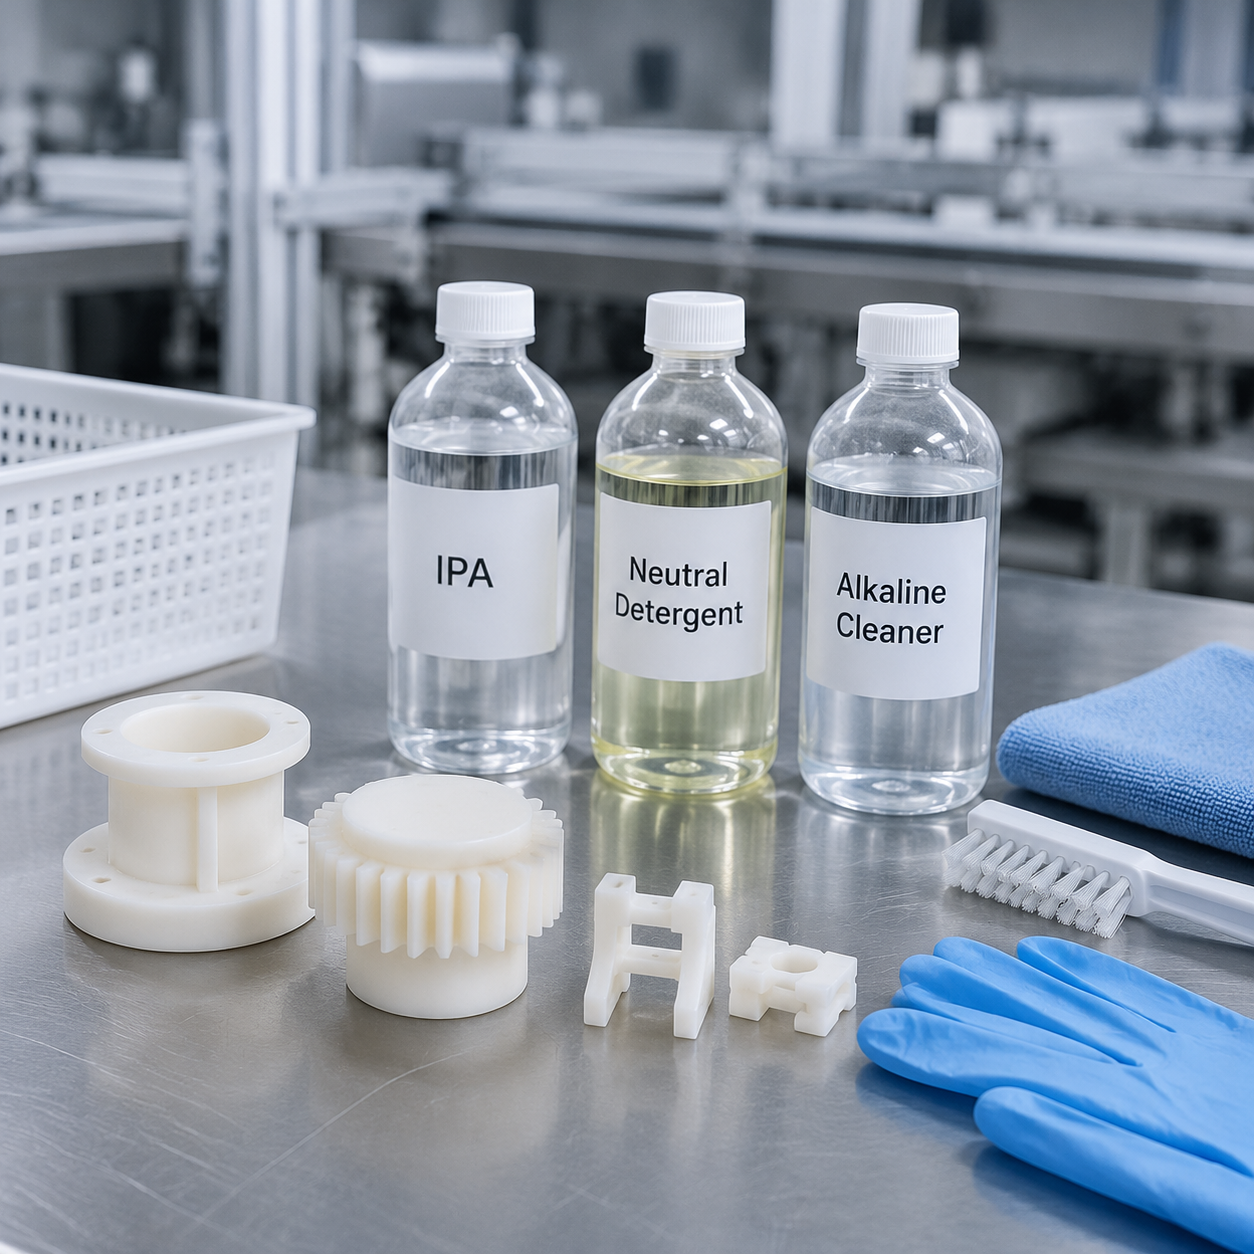
| Cleaner / Cycle | Nylon | Risk Level | Practical Note |
|---|---|---|---|
| IPA wipe | Often good | Low | Short contact is usually manageable. |
| Neutral detergent | Often good | Low | Good for normal maintenance cleaning. |
| Hot alkaline wash | Caution | Medium to high | Heat and soak time matter more than the label. |
| Bleach / oxidizers | Needs review | High | Do not assume compatibility for repeated use. |
| Solvent degreaser | Needs review | High | Test the actual blend, not just the main ingredient. |
| Steam or hot water wash | Caution | Medium to high | Hydrolysis can be the real failure mode. |
What Usually Fails First
The part rarely fails because of one quick wipe. It fails when a cleaning routine repeats under load, at elevated temperature, or with trapped moisture. That is why the service cycle matters more than the cleaner name.
Separate the Cleaner Families Before You Judge Nylon
A lot of bad approvals happen because teams treat all cleaners as one bucket. A brief IPA wipe is not the same as a hot alkaline wash. Neutral detergents, oxidizing disinfectants, solvent degreasers, and steam-assisted sanitation all stress nylon in different ways.
The practical question is not just “is nylon resistant?” but “what exactly touches the part, how hot is it, how long does it stay there, and does the part stay under load afterward?”
Practical Selection Rules
- Use nylon more comfortably for brief inspection cleaning than for repeated hot wash cycles.
- Check the full cleaning recipe: concentration, temperature, dwell time, and rinse step.
- If the part is stressed or dimension-critical, test the assembled part instead of a coupon only.
Validation Checklist for Repeated Cleaning
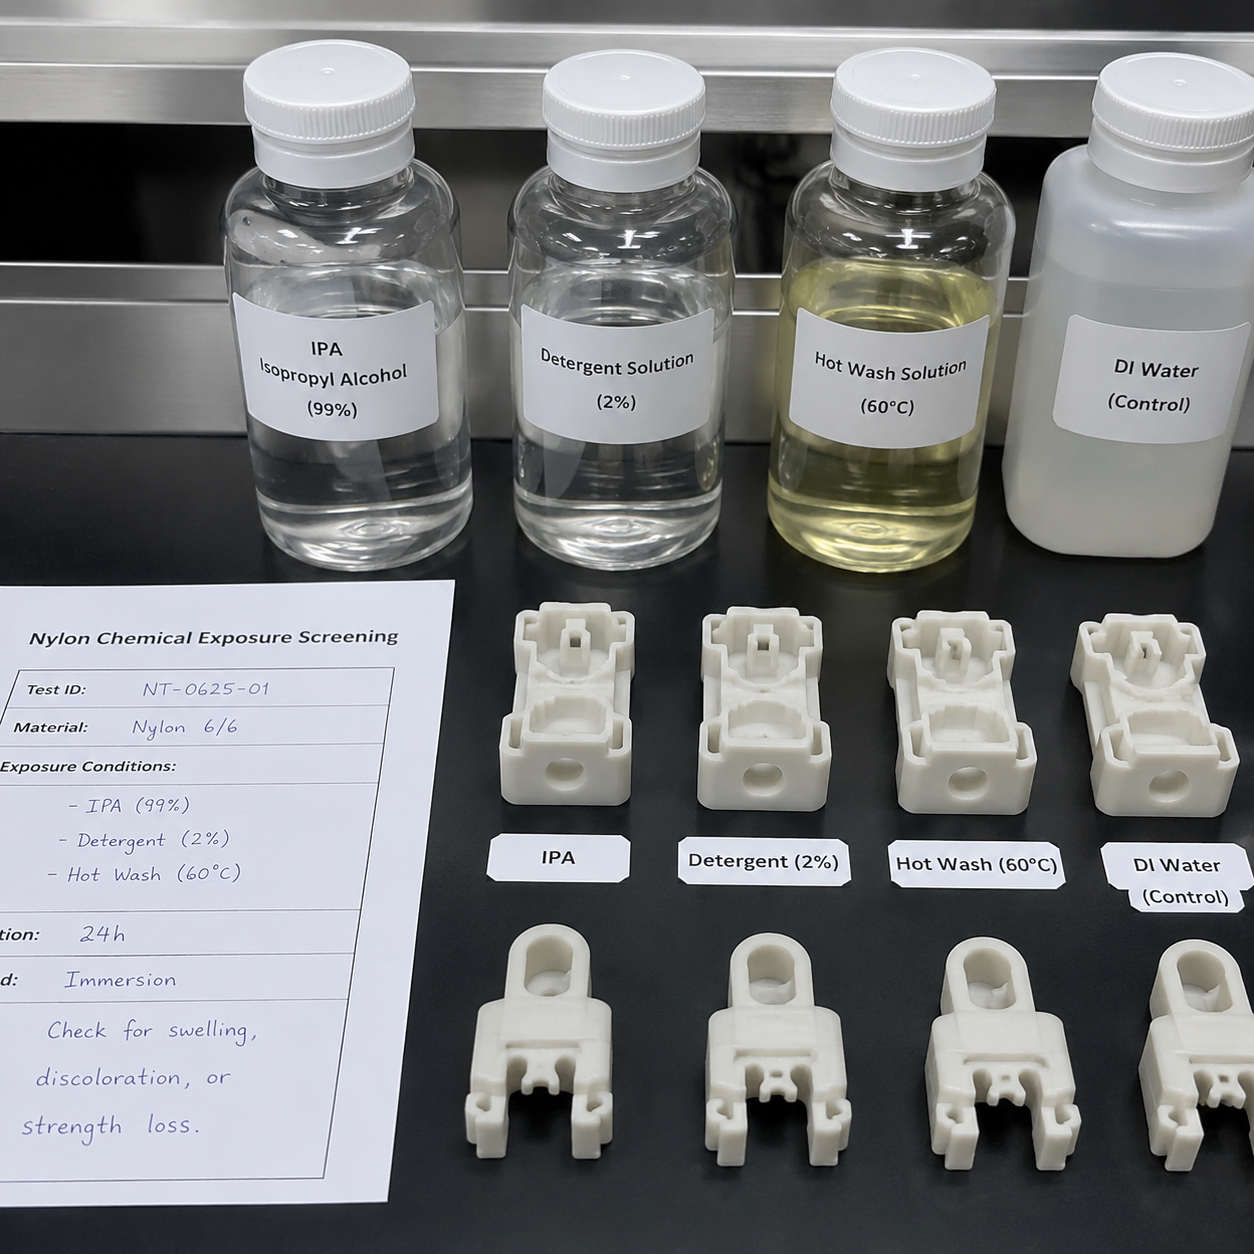
- Write down the exact cleaner, concentration, and dilution range used on the line.
- Separate wipe-down, foam soak, immersion, and spray wash as different exposure types.
- Check whether the part traps solution in ribs, hinges, blind holes, or assembled joints.
- Test after repeated cycles, not only after a single exposure.
- Watch for dimensional drift, clip force loss, embrittlement, and surface crazing.
Typical Application Example
A food equipment bracket that gets a quick IPA wipe at shift change is a very different case from a part that sees daily hot foam wash and alkaline rinse. In the second case, the wash recipe and cycle count matter more than the polymer name on the datasheet.
Related Reading
- Nylon hydrolysis resistance
- UV stabilized nylon outdoor weathering
- Nylon chemical resistance guide
- Engineering plastics compatibility chart
Why Repeated Wash Cycles Are Different From One-Time Exposure
A single wipe-down with IPA or neutral detergent rarely causes visible problems. The real risk accumulates over hundreds of cleaning cycles, especially when the part stays wet between cycles or dries incompletely. Each cycle brings fresh chemical contact, and any trapped solution continues to work between washes. For nylon, the combination of chemical exposure plus moisture absorption can double the dimensional movement compared to either factor alone.
Grade Matters: PA6 vs PA66 vs PA12 in Washdown Service
PA12 is often the first nylon grade to consider for repeated cleaning because its lower moisture absorption means less dimensional swing and slower chemical ingress. PA66 can work when stiffness and heat matter more than dimensional stability, but glass-filled grades may suffer from wicking along fiber interfaces. PA6 typically absorbs more moisture than PA66, making it the least predictable in wet cleaning environments. For any grade, hydrolysis-stabilized variants should be specified when hot water or steam is part of the cleaning cycle.
What to Monitor During Production Validation
Beyond visual inspection, production teams should track three metrics during cleaning cycle validation: dimensional drift (especially bore diameters and snap-fit gaps that may close or loosen after repeated conditioning), retention force on clips and press-fits that rely on polymer stiffness, and surface quality changes including micro-crazing that signals chemical attack before mechanical failure. Measuring after 5, 25, and 100 cycles gives a more reliable picture than a single post-exposure check.
FAQ
See our SAE PA66 properties and automotive grade selection for detailed property comparisons and application recommendations.
Is nylon safe with IPA?
Usually for brief cleaning contact, yes. Repeated soaking or hot cycles are a different case.
Can nylon handle alkaline cleaners?
Sometimes, but hot alkaline wash cycles can turn into a long-term problem even if the first test looks fine.
Is bleach safe for nylon parts?
Not something to assume. Oxidizing cleaners often need specific validation before production use.
What should I test before approving a wash cycle?
Test the actual cleaner, temperature, soak time, and the part while it is under load or installed in its final assembly.
If you are moving from material screening to production, review our nylon engineering plastics page for grade options, nylon injection molding services for molded parts, nylon CNC machining services for machined parts, and nylon 3D printing service for prototypes or low-volume functional parts.
Need a cleaning-cycle material review?
Send the cleaner, temperature, soak time, and part details. We can help check whether nylon is still the right choice.

