Nylon vs POM chemical resistance is usually not a simple winner-loser question. In real parts, moisture, temperature, load, and wear often matter as much as the fluid itself.
If you want the broader nylon view first, start with our nylon chemical resistance guide. If you need a wider cross-material screen, use the engineering plastics compatibility chart.
Bottom line: pick POM first when you need stable fit and low-friction motion in a wet but not extreme environment. Pick nylon first when load, impact, or higher heat is the bigger design problem.
At a Glance
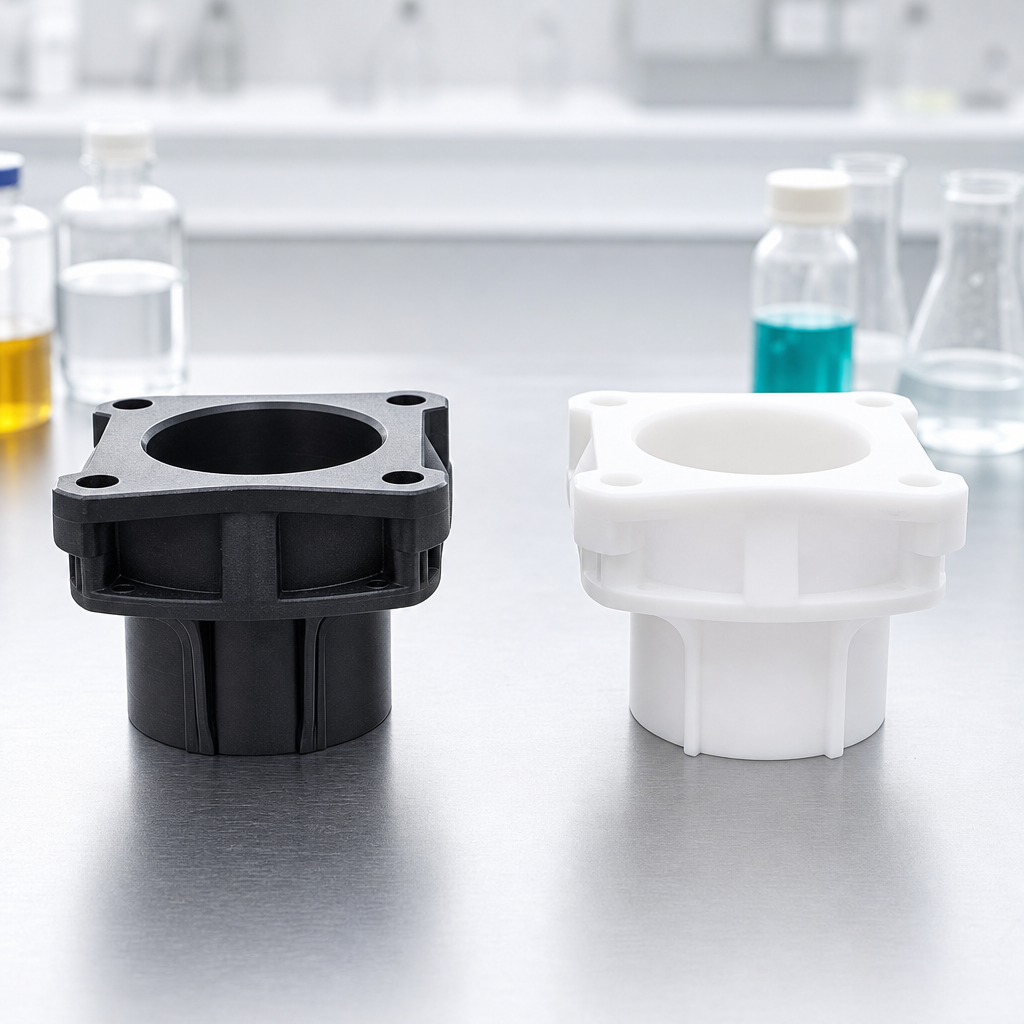
| Condition | Nylon | POM / Acetal | Usually Check First |
|---|---|---|---|
| Oils and greases | Often good | Often good | Both can work if temperature is controlled. |
| Fuels | Grade dependent | Often good | POM often looks cleaner on shortlists. |
| Hot water / humidity | Moisture sensitive | More stable | POM when dimensional stability matters. |
| Alkaline cleaners | Caution | Caution | Check concentration and soak time. |
| Strong acids | Poor | Poor | Consider another polymer first. |
| Dry-running wear | Tough and durable | Low friction and stable | POM often wins on sliding feel. |
Where Nylon Usually Wins
Nylon usually comes back into the shortlist when the part needs toughness, impact tolerance, or better heat headroom than a purely low-friction grade. If the part is carrying a load, flexing, or seeing repeated shock, nylon can be the more forgiving choice.
Where POM Usually Wins
POM often looks better when the part must keep size, slide smoothly, and stay predictable in a dry or lightly lubricated assembly. It is also a common first check when moisture uptake is hurting fit more than chemistry is.
Failure Modes That Usually Decide the Choice
When teams choose between nylon and POM, the first failed sample often tells the real story. Nylon usually gives up through swelling, dimensional movement, or loss of repeatability after moisture and fluid exposure combine. POM more often leaves the shortlist when impact, heat, or long-term creep under load become more important than low-friction stability.
- Nylon risk: bore growth or fit shift after conditioning, especially in humid service.
- POM risk: lower confidence in higher-heat structural loading when the geometry is thin or highly stressed.
- Shared risk: both materials can still fail in strong acids, hot oxidizing cleaning cycles, or poorly controlled solvent exposure.
Engineering Rule
Use nylon when you need a tougher structural part. Use POM when you need a more dimensionally stable wear part. If chemical exposure is the main issue, test the actual fluid, temperature, and dwell time before deciding.
What To Validate Before Tooling
A material comparison only becomes useful when it is tied to the real assembly. For nylon vs POM, the practical review should include more than the fluid name.
- Whether the part is load-bearing, snap-fit, or only positional.
- Installed clearance before and after humidity or fluid conditioning.
- Shaft finish, lubrication method, and dry-running duty for wear parts.
- Maximum service temperature, not just room-temperature exposure.
- Cycle type: splash, wipe, soak, or continuous contact.
Typical Application Example
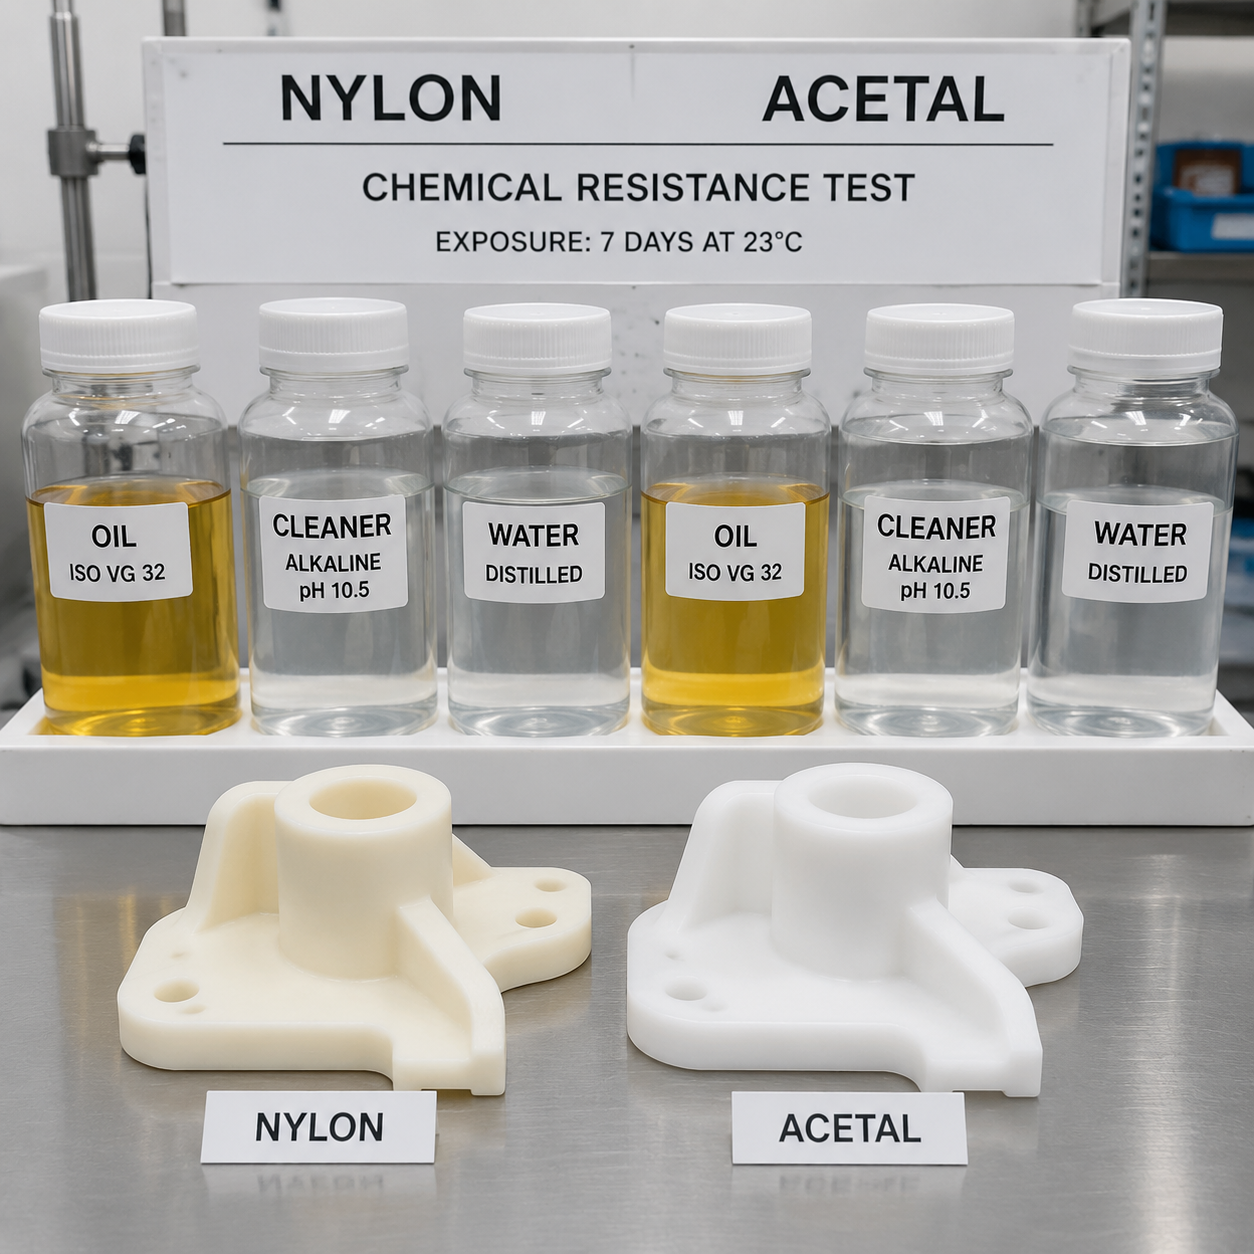
A small bush or spacer running dry inside a lightly lubricated mechanism is often a POM-first conversation because dimensional stability and sliding feel matter most. A clip, bracket, or structural support with the same fluid exposure may still stay in nylon territory if it needs more toughness or heat margin.
Related Reading
- Nylon chemical compatibility chart
- Nylon chemical resistance guide
- POM injection molding guide
- Nylon moisture absorption
Wear Rate Comparison Under Realistic Loading
In dry-sliding conditions, POM typically shows 30 to 50 percent lower wear rates than unfilled nylon because its surface energy is lower and its crystalline structure provides natural lubricity. However, adding glass fiber to nylon can close this gap significantly: nylon 66 GF30 often matches POM wear rates in lightly loaded sliding applications while providing higher load-carrying capacity. The trade-off is that glass-filled nylon wears the mating surface faster than unfilled POM, so the counterface material choice becomes part of the material decision.
Cost-Performance Trade-offs in Production Volumes
At moderate volumes, the raw material price difference between nylon and POM is often small enough that engineering performance should drive the choice rather than resin cost. However, two hidden costs can tip the balance: conditioning time (PA66 parts may need post-molding moisture conditioning to reach target dimensions, adding days to production flow) and tooling complexity (POM’s higher shrinkage and narrower processing window can require tighter mold temperature control). For parts above 50,000 units per year, the combined cost difference including processing, conditioning, and scrap can exceed 15 percent, making the earlier material decision more consequential than the price-per-kilogram comparison suggests.
When Neither Is Right: PBT as the Third Option
When nylon loses too much dimension to moisture and POM falls short on heat or toughness, PBT often enters the conversation. PBT offers moisture stability close to POM with better electrical properties and lower creep than unfilled nylon. It is worth screening early when the application sits in the overlap zone: tight tolerances needed, occasional hot-wet exposure present, and wear rate secondary to dimensional control. See our nylon vs PBT guide for a direct comparison when chemical exposure is the main concern.
FAQ
Compare detailed PA66 GF30 properties and grade selection across GF15, GF30 and GF60 glass fiber reinforcement levels in our dedicated glass-filled nylon guide.
Is POM more chemical resistant than nylon?
Sometimes, especially where moisture and dimensional stability matter. But the answer depends on the exact chemical, temperature, and load.
Is nylon better than acetal for wear parts?
Nylon is often tougher, while POM is often more stable in sliding use. The better choice depends on whether impact or low-friction repeatability matters more.
Can nylon replace POM in chemical contact?
Yes in some cases, but not by default. Check the fluid, soak time, and whether the part is loaded or dimension-critical.
When should both be avoided?
Strong acids, aggressive oxidizers, and hot wash cycles usually push both materials out of the first-choice range.
If you are moving from material screening to production, review our nylon engineering plastics page for grade options, nylon injection molding services for molded parts, nylon CNC machining services for machined parts, and nylon 3D printing service for prototypes or low-volume functional parts.
Need a material comparison review?
Send the fluid, temperature, load, and part geometry. We can help compare nylon and acetal before tooling starts.

