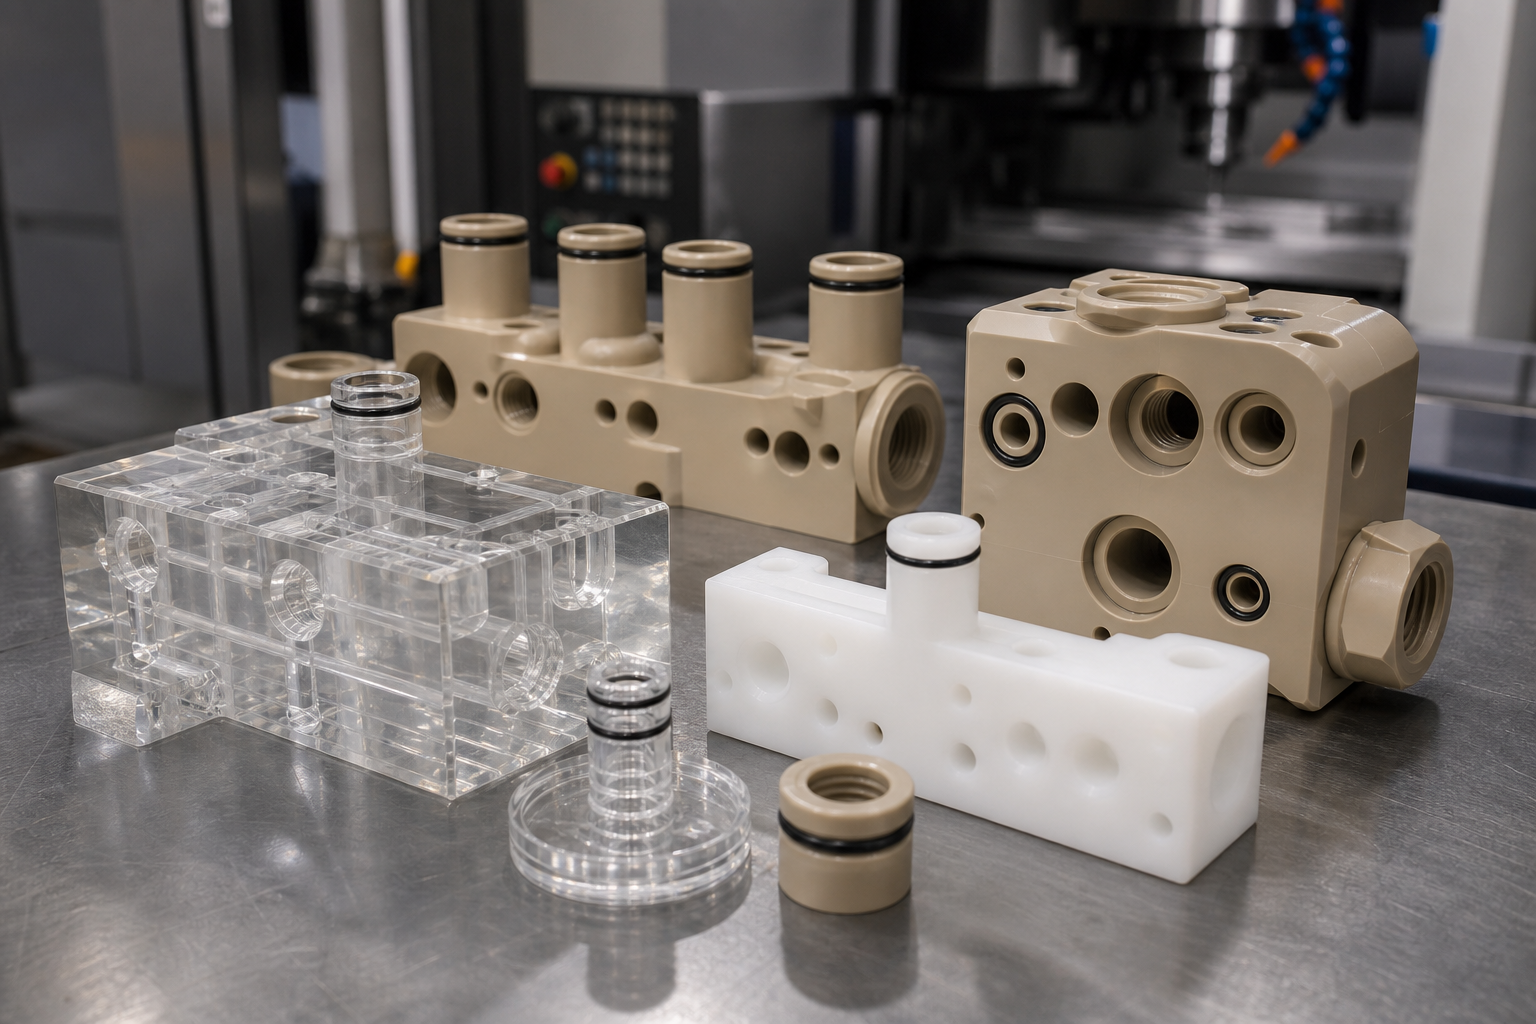
Plastic manifold manufacturing is really leak control under geometry constraints. If the internal path, sealing land, port orientation or resin choice is wrong, the part may still look fine while quietly becoming the weak link in the system.
That is why the usual first step is to decide whether the manifold should be machined, molded or reworked in stages. On most new programs, CNC is the safer starting point because port layout and sealing details still change during validation.
For fluid, pneumatic, analytical and process equipment teams
What a Capable Manifold Supplier Should Review
The supplier should review media, pressure, temperature, flow path, sealing, cleaning and inspection before confirming material or manufacturing route.
- Material: match chemical and temperature exposure, not only pressure
- Geometry: check intersecting channels, plugs, dead legs and tool access
- Validation: define pressure, leak and cleanliness requirements in the RFQ
At a Glance
| Decision Point | Why It Matters | Buyer Check |
|---|---|---|
| Fluid compatibility | Controls swelling, stress cracking and service life | List every media and cleaning chemical |
| Port and thread design | Drives assembly and leakage risk | State fitting standard and torque |
| Internal channels | Affect pressure drop and cleanability | Share flow and dead-volume targets |
| Manufacturing route | Changes tooling cost and revision flexibility | Start with machining for unstable designs |
| Leak testing | Confirms the complete sealing system | Define method, pressure and acceptance limit |
Designing Internal Channels, Ports and Seals
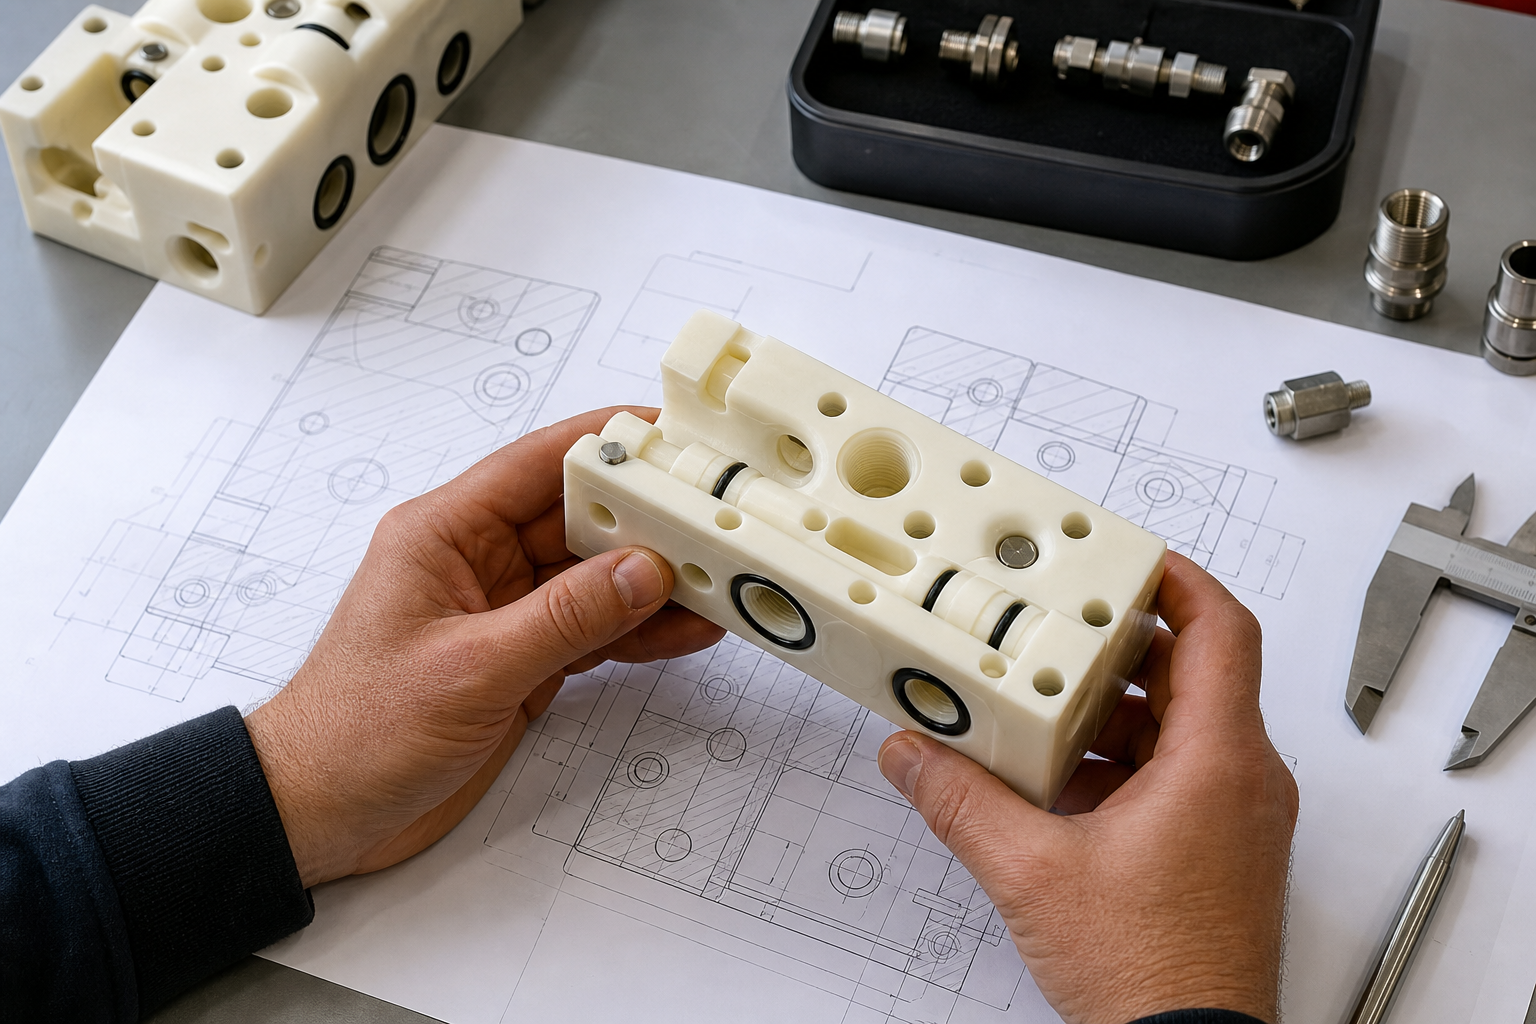
Cross-drilled passages often require plugs, while more complex channel networks may use bonded layers or multiple components. Each method changes cleanability, pressure capability and inspection access. The design should make the flow path understandable to both manufacturing and quality teams.
Threads in plastic need sufficient engagement and controlled assembly torque. O-ring glands must consider material stiffness, surface finish, compression and tolerance stack. A nominally correct groove can still leak if the adjoining port, plug or mating face is not controlled.
RFQ Checklist for a Custom Plastic Manifold
- List all fluids: include concentration, temperature, exposure time and cleaning media.
- Define pressure conditions: provide normal, peak, vacuum and test pressure.
- Identify every port: include standard, size, fitting type, torque and orientation.
- State cleanliness needs: particle, flushing and packaging requirements affect the process.
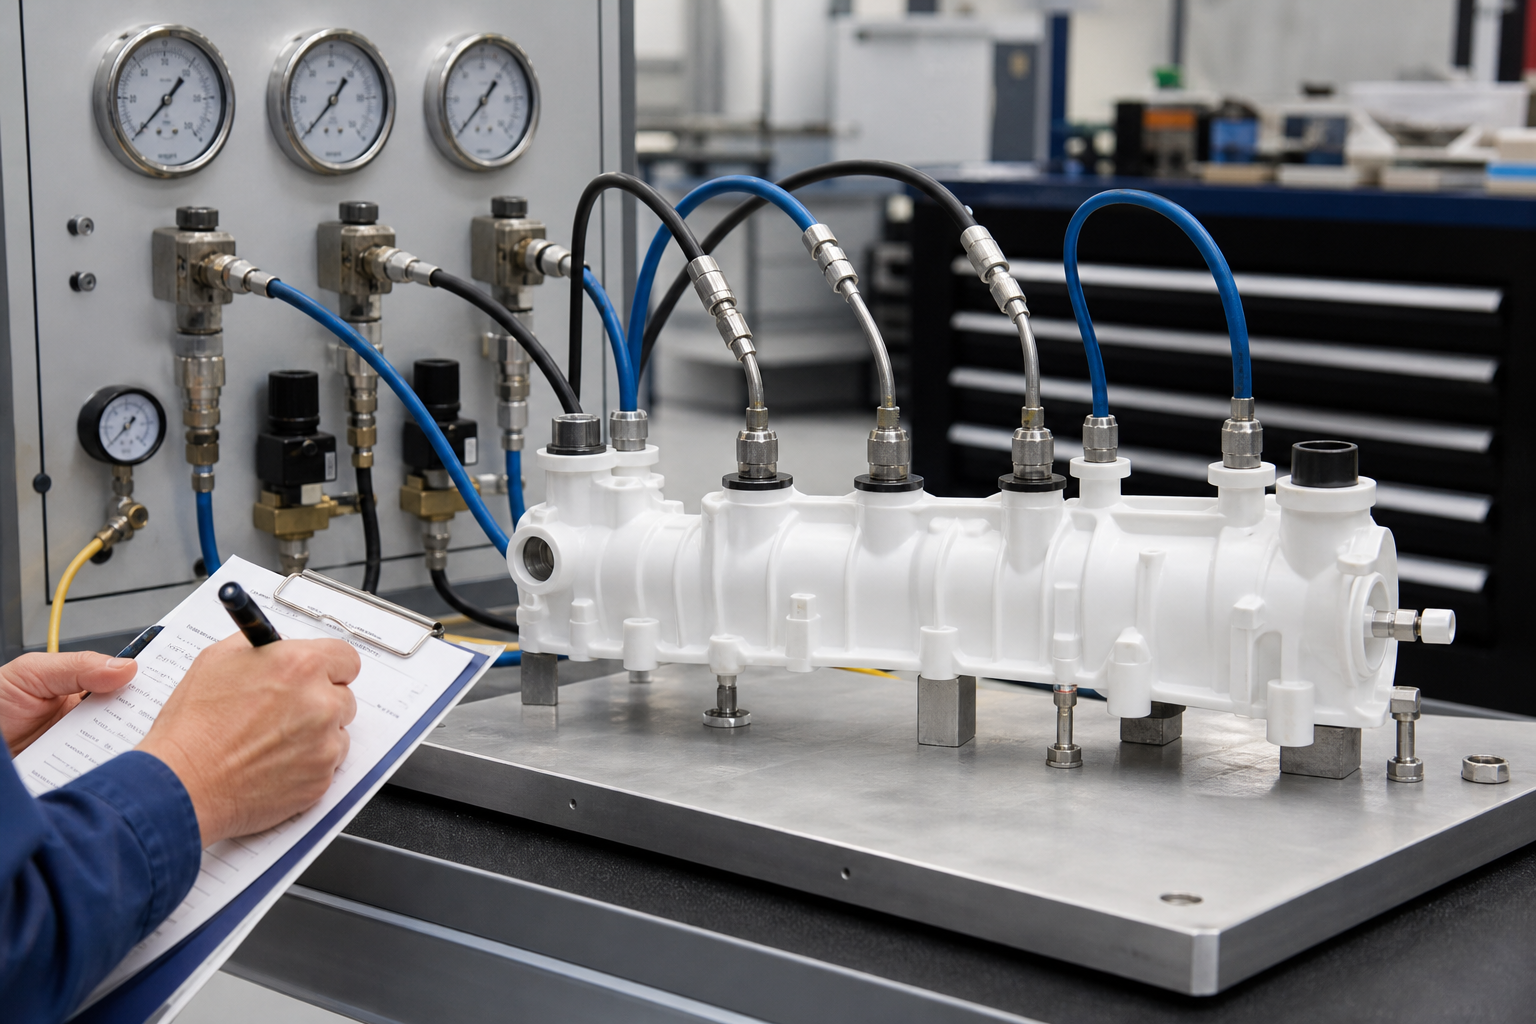
- Provide test acceptance: define leak method, duration, pressure and documentation.
Application and Manufacturing Matrix
| Application | Recommended Direction | Important RFQ Detail |
|---|---|---|
| Analytical instrument | Machined PEEK, PPS, PC or acrylic manifold | Dead volume, cleanliness and chemical exposure |
| Water or chemical system | Machined PVC, PP, HDPE or PVDF block | Media, pressure and joining method |
| Pneumatic control | Machined POM or engineering-plastic manifold | Port standard, pressure and thread life |
| Higher-volume stable assembly | Evaluate molded or hybrid manifold | Tooling, inserts, sealing and validation cost |
Common Project Risks and Practical Fixes
| Risk | Why It Happens | Practical Fix |
|---|---|---|
| Leak at threaded port | Thread engagement, torque or material creep is unsuitable | Review fitting standard and assembly load |
| Internal contamination | Dead legs, burrs or cleaning access were ignored | Design for deburring, flushing and inspection |
| Stress cracking | Material is incompatible with fluid or assembly stress | Validate media, temperature and fitting torque together |
| Unexpected pressure drop | Channel diameter and routing do not match flow needs | Review flow path before releasing the drawing |
Machined, Bonded or Molded Plastic Manifolds
Machined manifolds offer the fastest revision cycle and avoid tooling, which makes them suitable for prototypes and recurring low-to-medium volumes. Bonded-layer designs can create complex planar channels but require a validated joining process.
Molded manifolds can reduce unit cost at volume, yet tooling makes channel revisions expensive. The safest path is to validate fluid, port and seal behavior in a machined design before investing in production tooling.
Need a design-for-leak-test review?
Send the manifold model, fluid list, pressure, port schedule, sealing method and quantity. We can identify material, tool-access and test risks before quoting.
Why Choose Nylon Plastic
Nylon Plastic supports engineering-plastic selection, CNC machining, molding review and dimensional inspection for custom fluid components. Buyers can evaluate the complete route from prototype manifold to repeat production.
Manifold Route Selection: Machined, Molded or Bonded
| Route | Useful When | Risk to Resolve |
|---|---|---|
| CNC machined block | Channels, ports or revisions are still being validated | Tool access, cross-drilling plugs, sealing, burrs and dimensional stability |
| Molded manifold | Geometry and annual volume justify dedicated tooling | Core design, weld lines, shrinkage, inserts, leak testing and tool changes |
| Bonded or assembled pieces | Internal paths are difficult to machine as one block | Joint strength, chemical exposure, alignment, cleanliness and long-term leakage |
| Modified nylon option | Strength, wear or weight matters in a suitable fluid and temperature range | Moisture, chemical compatibility, creep, thread load and exact grade documentation |
A manifold can pass an initial pressure test and still fail through thread creep, seal relaxation, solvent exposure, trapped chips or a port that cannot be serviced. Define the fluid, pressure, temperature, duty cycle, cleanliness, fitting torque, leak-test method and inspection state before deciding whether machining or molding is the economical route.
How Nylon Plastic Supports Manifold Projects
Nylon Plastic supports material review, CNC machining, injection molding and inspection for custom plastic fluid components. The team can compare unfilled PA, PA-GF20 or PA-CF30 with other plastics when the required stiffness, chemical resistance, dimensional stability and leak performance justify the choice.
- Review internal channel access, port orientation, sealing lands, inserts and inspection datums before quotation.
- Define leak-test medium, pressure, duration, acceptance limit, cleanliness and traceability in the RFQ.
- Use a machined validation part before committing to molding when the channel layout or fluid qualification is still changing.
Related Reading
Frequently Asked Questions
What does a plastic manifold manufacturer need for a quote?
Provide the 3D model, drawing, fluid list, pressure, temperature, port specifications, sealing method, cleanliness target, quantity and leak-test requirement.
Which plastics are used for fluid manifolds?
Options can include POM, PEEK, PPS, PP, HDPE, PVC, PVDF, PTFE, acrylic and suitable nylon grades. The exact fluid, pressure, temperature and approval route determine the choice.
Should a custom manifold be machined or molded?
Machining is often useful for validation and lower volume. Molding becomes attractive after channels, ports, material, annual demand and qualification requirements are stable.
How are custom plastic manifolds leak tested?
Use the specified medium, pressure, duration, temperature and acceptance limit. Record the part revision, test equipment, operator, result and any conditioning state.
Can a plastic manifold use threaded metal fittings?
It can, but thread engagement, torque, insert retention, creep, thermal cycling, chemical exposure and sealing method must be designed for the exact plastic and service condition.
Request a Plastic Manifold Review
Send the model, fluid and pressure conditions, port schedule, seals, quantity, cleanliness target and test standard for a material and manufacturing-route review.