PTFE CNC machining services are usually selected for sealing, chemical resistance, electrical isolation and low-friction applications. Buyers often know PTFE by the Teflon name, but the important engineering reality is that PTFE behaves very differently from stiffer plastics during machining, inspection and use.
The biggest mistake is treating PTFE like POM or nylon. It is softer, more prone to creep and more likely to move under clamping or after release. A supplier that machines PTFE well plans around material deformation, not just toolpath geometry.
At a Glance
| Decision Point | PTFE Machining Takeaway | Buyer Note |
|---|---|---|
| Chemical resistance | Usually excellent | Useful for harsh media and sealing systems |
| Friction behavior | Very low friction | Good for slides, seats and non-stick surfaces |
| Tolerance stability | More difficult than rigid plastics | Define realistic tolerances by function |
| Load performance | Can creep under stress | Filled PTFE may be better for wear and deformation control |
| Best fit | Seals, valve seats, chemical parts, electrical insulators | Not ideal where stiffness is the first priority |
For sealing and chemical-service parts
Select PTFE for the Service Conditions
The real question is whether virgin PTFE, filled PTFE or another fluoropolymer is the right material for the load, tolerance and wear profile. Good PTFE sourcing starts with function, not the brand name.
- Use virgin PTFE for purity and chemical resistance
- Use filled PTFE when creep or wear becomes a problem
- Set functional tolerances for seals and soft parts
What Buyers Need to Know About PTFE Machining
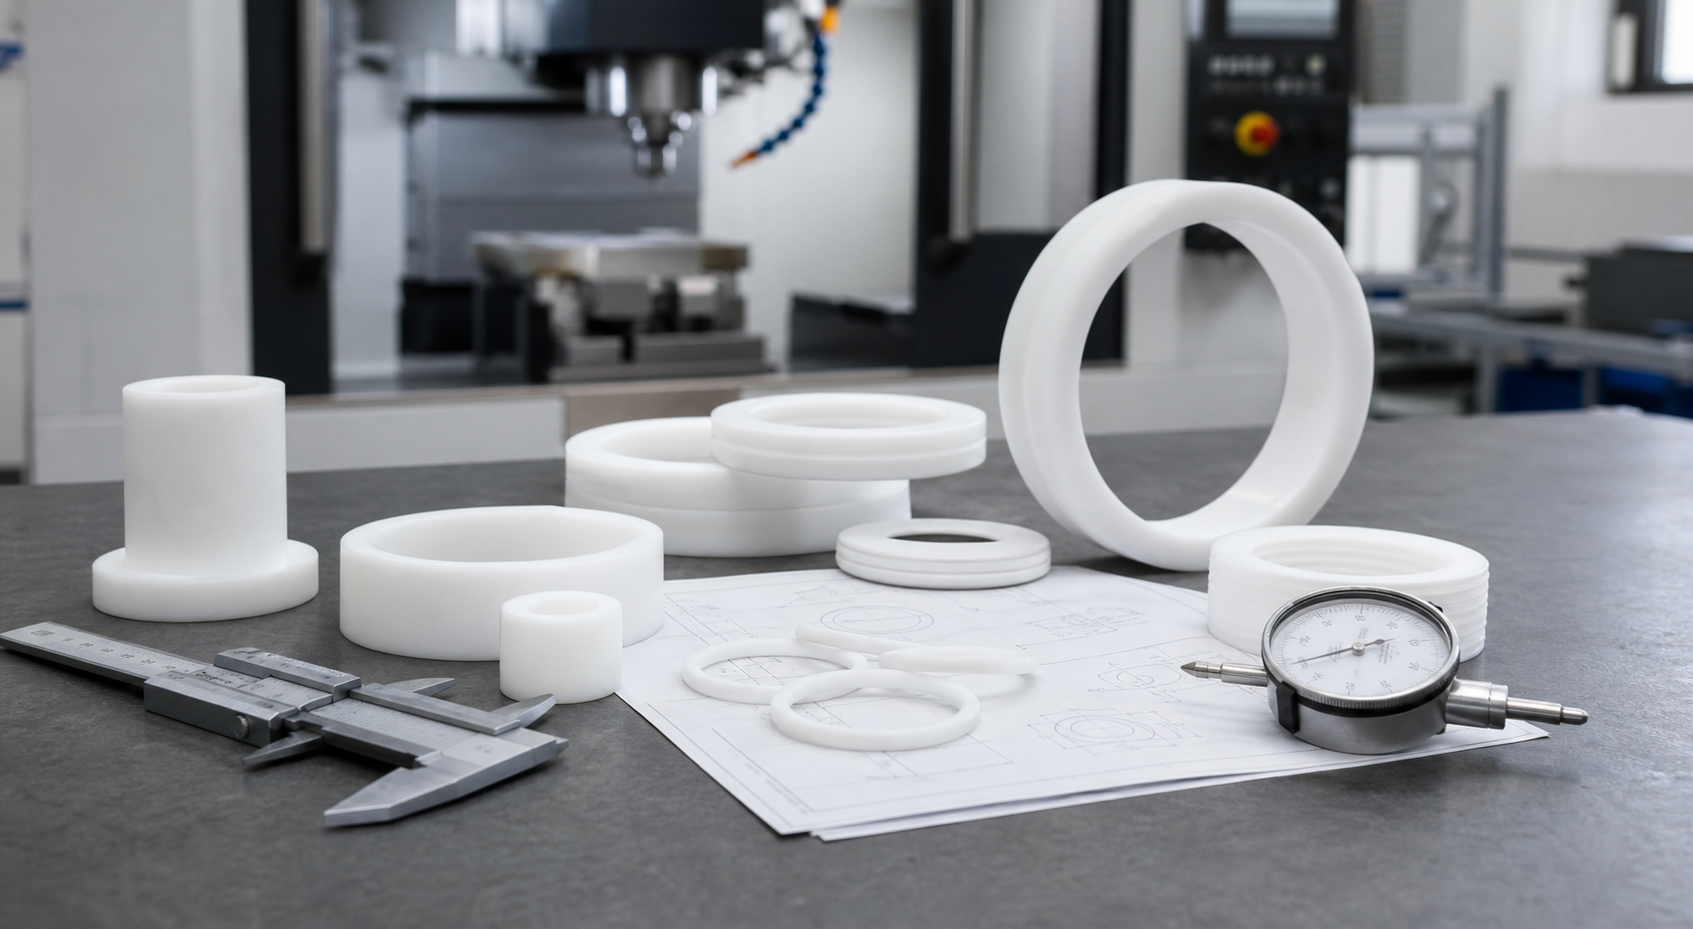
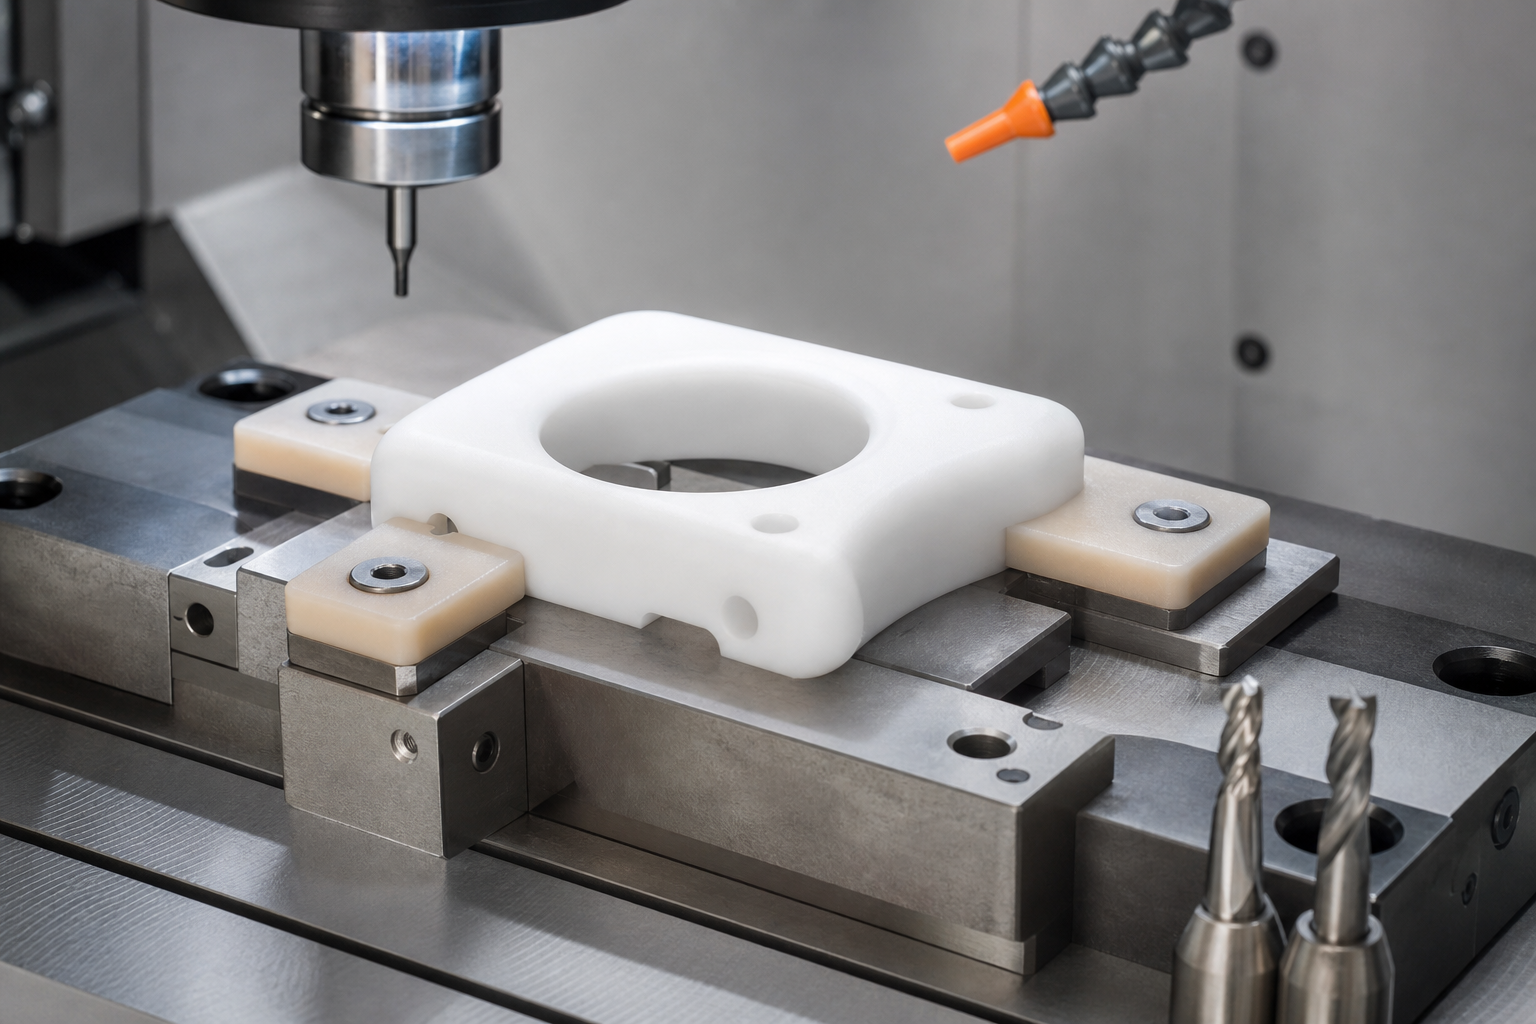
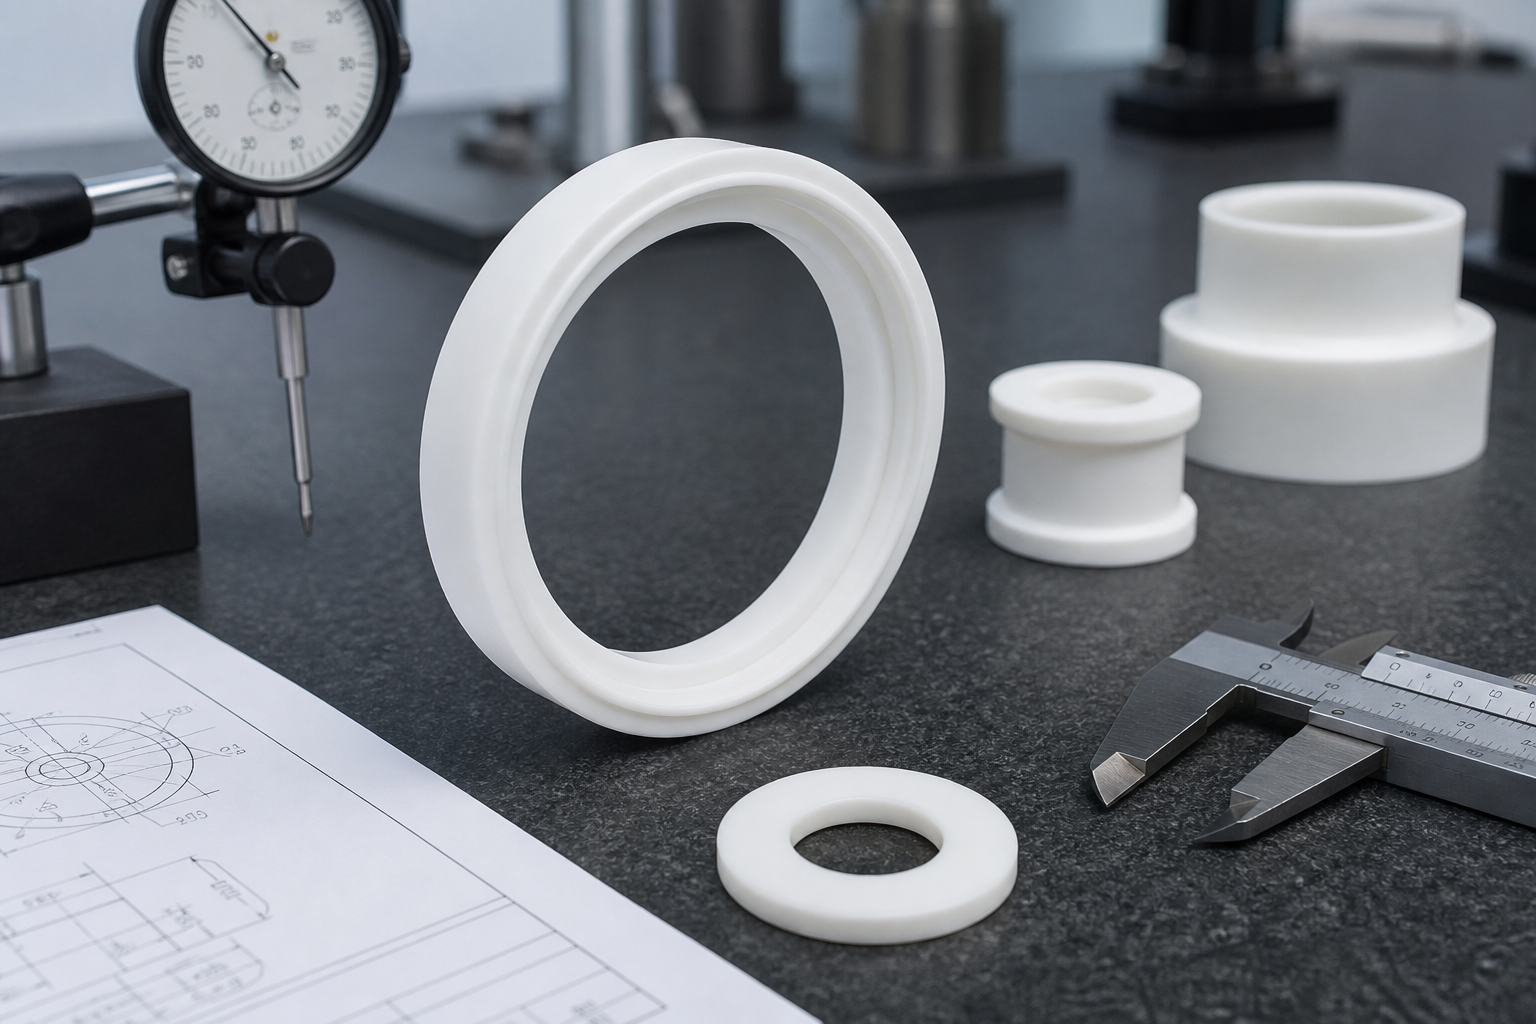
PTFE can deform during workholding, and the part may recover slightly after unclamping. That means the supplier has to control how the part is held, how much material is removed in each stage and when the final measurement is taken. On softer ring, seal and seat components, inspection method matters almost as much as machining method.
Filled PTFE grades, such as glass-filled or carbon-filled PTFE, can improve wear or compressive behavior, but they also change machinability, electrical properties and media compatibility.
Common PTFE Machining Risks and Practical Fixes
| Risk | Why It Happens | Practical Fix |
|---|---|---|
| Out-of-tolerance after release | Soft material recovers after fixturing | Use low-distortion workholding and appropriate measurement timing |
| Creep in service | PTFE deforms under long-term load | Use filled PTFE or redesign support where needed |
| Wrong material grade | Virgin PTFE selected for a wear-heavy duty | Compare filled grades early in the RFQ stage |
| Overly tight quoting assumptions | PTFE treated like a rigid engineering plastic | Set realistic tolerances by sealing or function requirement |
PTFE vs Other Machined Plastics
PTFE is not a general replacement for POM, nylon or UHMW. Choose PTFE when chemical exposure, low friction or high-purity requirements dominate. Choose another plastic when stiffness, load support or easier tolerance control is more important.
Related Reading
- Custom Machined Plastic Parts
- Chemical Resistance Guide for Engineering Plastics
- PTFE vs PEEK Comparison
- CNC Plastic Turning Services
- Engineering Tolerance Guide for Plastic Parts
- CNC Machining Services
Frequently Asked Questions
When should I use PTFE CNC machining services?
Use them for chemical-service, low-friction, sealing or insulating parts where PTFE properties matter more than stiffness.
Can PTFE hold tight tolerances?
It can hold practical functional tolerances, but it is usually more difficult than rigid plastics because PTFE can deform during workholding and use.
Should I choose virgin or filled PTFE?
Choose virgin PTFE for purity and broad chemical resistance. Choose filled PTFE when creep, wear or compressive performance needs improvement.
What should I send for a PTFE machining quote?
Send the drawing, fluid exposure, temperature, tolerance, sealing function and quantity so the grade and process can be screened properly.
Is PTFE the best choice for every low-friction part?
No. UHMW, POM and other plastics may be better when the part needs more stiffness or simpler dimensional control.
Request a PTFE Machined Parts Review
Nylon Plastic helps buyers separate material reputation from actual application fit. That is especially important with PTFE, where performance can be excellent in the right environment but disappointing if stiffness or load demands were underestimated.
For custom seals, valve seats, bushings or insulators, send the current CAD and drawing revision, quantity and required delivery destination. For material selection only, identify the current grade, stock form and service conditions; a part drawing is useful when dimensional fit also needs review.
- Grade and service: manufacturer and exact virgin or filled PTFE grade, permitted alternatives, fluid or cleaning-media exposure, temperature and whether the part seals, slides or insulates.
- Fit and acceptance: mark sealing faces and critical dimensions, permitted edge breaks and surface requirements. Agree measurement method, relaxation time and inspection temperature. For a seal, specify mating geometry, pressure and the required leak test; dimensional inspection alone does not approve sealing performance.
- Order and records: prototype or repeat-order quantity, material traceability and inspection records, cleaning or packaging requirements, destination and target timing.
The review can identify grade, drawing and inspection questions before quotation. Compare quotes for the same stock, machining, edge treatment, inspection and packaging scope, with assumptions and exclusions stated. Any sample or service test required for approval should be agreed separately.