PPA CF vs PET CF is a high-performance comparison between a hotter-running engineering material and a more accessible carbon-filled polyester route. Teams usually compare them when standard PA6-CF or PETG-CF grades are no longer enough for the temperature or stiffness target.
The better choice depends on whether the part needs higher heat capability and stronger engineering credibility, or whether it needs a more economical carbon-filled option with fewer processing penalties.
This page is for a high-heat two-material decision. If the team is still making a broader carbon-fiber filament choice across PA6-CF, PET-CF and PC-CF, use the parent comparison first: PA6-CF vs PET-CF vs PC-CF.
At a Glance
| Decision Factor | PPA-CF | PET-CF | Buyer Note |
|---|---|---|---|
| Heat resistance | Usually much higher | Moderate | PPA-CF is often chosen for hotter engineering environments |
| Print difficulty | Higher | Lower | PPA-CF requires a stronger process setup |
| Structural stiffness | High | High | Both can serve rigid part roles, but not at the same temperature limit |
| Commercial accessibility | More specialized | Easier | PET-CF is often the easier route for lower-risk builds |
| Best fit | Higher-heat engineering parts | General rigid carbon-filled prototypes | Choose by service temperature first |
When PPA-CF Is Worth the Extra Complexity
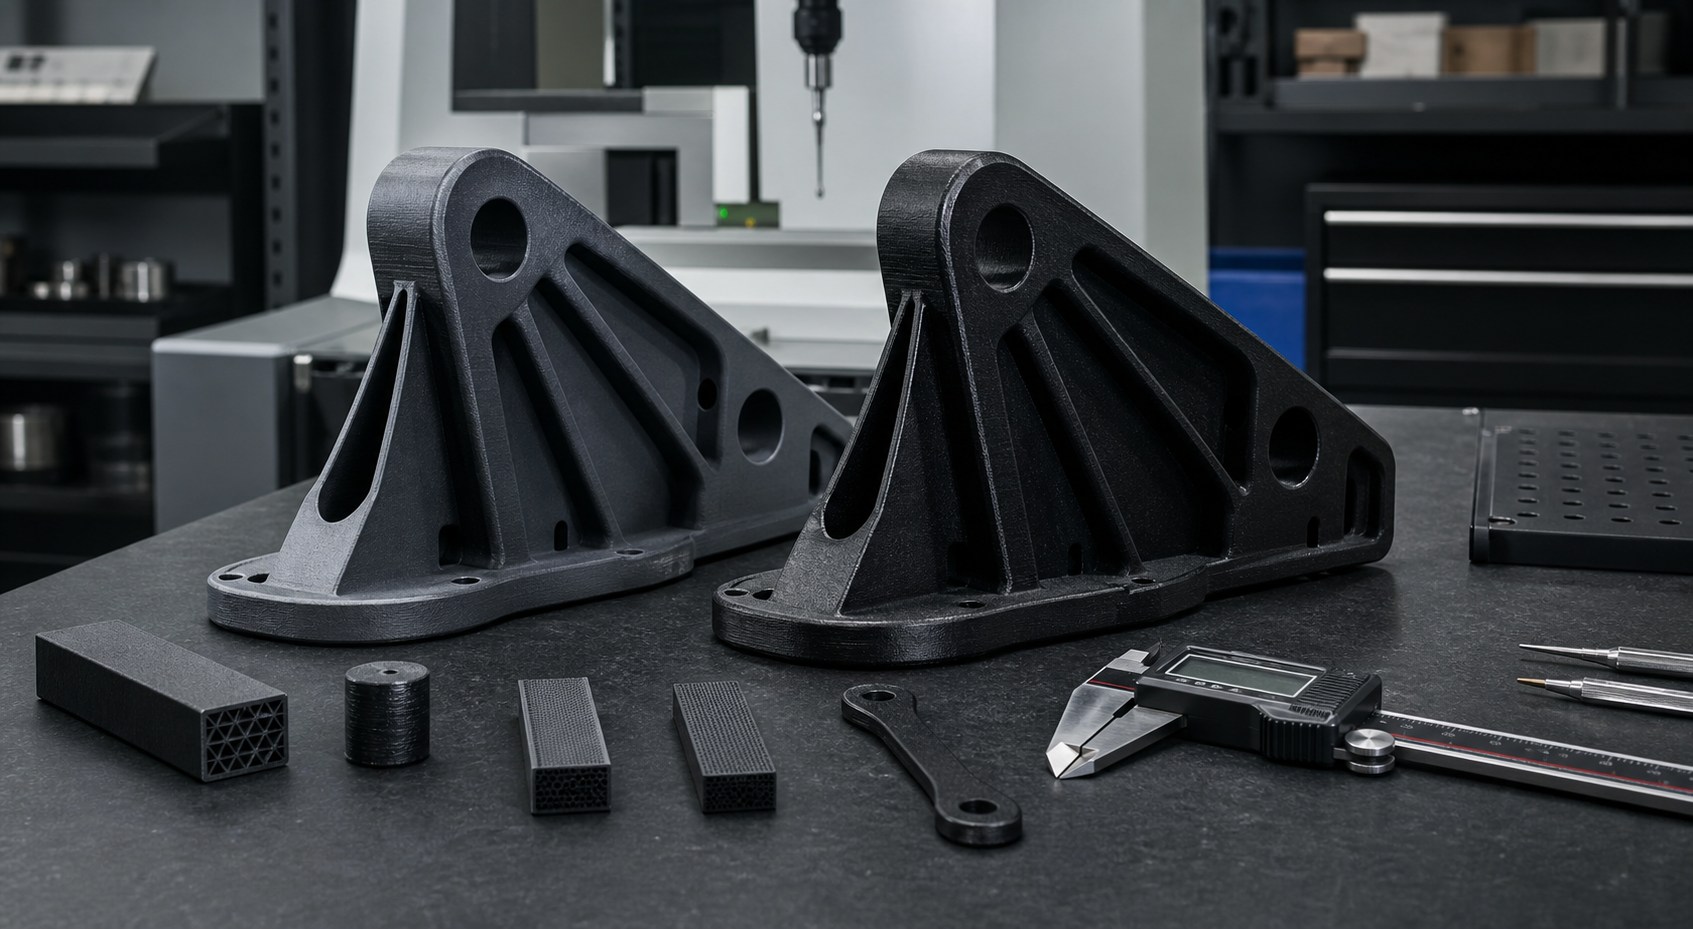
PPA-CF is usually selected for under-hood, hotter enclosure and mechanically demanding parts where a more advanced engineering polymer is needed. It is often a better fit when the printed part is expected to stand in for a higher-heat molded engineering resin during validation.
When PET-CF Is the Better Commercial Choice
- The temperature requirement is moderate: PET-CF may be enough without moving into a harder print workflow.
- The part needs rigidity more than extreme heat capability: PET-CF can be a lower-risk answer.
- The team needs lower development cost: PET-CF is usually more accessible than PPA-CF.
- The build is for functional prototyping rather than severe environment validation: PET-CF may be the more efficient route.
Common PPA-CF vs PET-CF Mistakes
| Mistake | Risk | Better Approach |
|---|---|---|
| Choosing PET-CF for a higher-heat requirement | Part softens or drifts in service | Set the actual service temperature before locking the material |
| Choosing PPA-CF without the printer capability | High scrap and unstable results | Confirm chamber, nozzle and drying readiness first |
| Using carbon fiber as the main decision point | Base polymer limits are missed | Choose the resin family before the filler story |
| Ignoring cost of iteration | Prototype budget rises too fast | Use PPA-CF only when the application truly needs it |
PPA-CF vs PET-CF for Engineering Procurement
If the part must represent a hotter or more demanding engineering application, PPA-CF is often the correct route. If the part needs a stiff carbon-filled prototype without extreme heat demands, PET-CF can be the more efficient commercial choice.
Why Choose Nylon Plastic
Nylon Plastic helps teams decide whether a high-heat carbon-filled route is technically necessary or whether a simpler carbon-filled material will satisfy the real project requirement.
Related Reading
- PPA Material Guide
- High-Temperature Engineering Plastics
- PA6-CF vs PET-CF vs PC-CF
- Plastic 3D Printing Services
- PC Filament Guide
Processing Temperature Requirements: The Real Gate Between These Materials
The practical dividing line between PPA-CF and PET-CF is often the printer’s hot-end and chamber capability, not the data sheet numbers. PPA-CF typically requires a nozzle temperature above 280°C and a heated chamber approaching 80-100°C for reliable layer adhesion. PET-CF can generally be printed at 250-270°C with chamber temperatures below 70°C. A printer that runs PET-CF successfully may still be unable to produce dimensionally stable PPA-CF parts. Before committing to PPA-CF, verify that the printer’s thermistor, heater cartridge, and firmware can sustain the required temperature envelope through the full build duration, not just for the first few layers.
Post-Processing Differences: Annealing Requirements
Both PPA-CF and PET-CF benefit from annealing, but the requirements differ substantially. PPA-CF parts typically need a controlled ramp to 120-150°C held for 2-4 hours to relieve internal stresses and stabilize crystallinity, while PET-CF annealing is usually adequate at 80-100°C. Skipping this step on PPA-CF can leave the part 20-30 percent below its rated heat deflection temperature and susceptible to warpage during service. The annealing fixture and support strategy must be defined before the build, not as an afterthought.
Cost-Per-Part Breakdown: When the Price Gap Matters
PPA-CF filament typically costs 2 to 3 times more per kilogram than PET-CF, but the per-part cost gap is often wider because PPA-CF’s higher scrap rate and longer print times amplify the difference. For a batch of 20 functional prototypes, the total cost including material, printer time, post-processing, and failed builds can run 3 to 5 times higher for PPA-CF. This cost multiplier is justified when the part genuinely needs high-heat performance, but it represents wasted budget when PET-CF would have met the thermal requirement. Teams should estimate both the material cost and the process yield before choosing.
Frequently Asked Questions
Compare nylon vs polycarbonate comparison including strength, heat, cost and application recommendations.
Is PPA-CF better than PET-CF for heat?
Usually yes. PPA-CF is generally chosen when the part must tolerate higher temperatures or a more demanding engineering environment.
Why not use PPA-CF for every carbon fiber part?
Because it usually carries higher print difficulty and cost, which are not justified unless the application really needs the performance.
When is PET-CF enough?
PET-CF is often enough for stiff functional prototypes and lower-risk engineering builds where extreme heat capability is not required.
What is the main risk with PPA-CF?
The main risk is choosing it without the printer capability and process control needed to run it consistently.
What should I send for a PPA-CF vs PET-CF recommendation?
Send the model, service temperature, load requirement and whether the printed part is a prototype proxy or a low-volume end-use component.
Send the part requirement if you want help deciding whether PPA-CF is necessary or PET-CF is enough.