PEEK (polyetheretherketone) sits at the apex of engineering thermoplastics: continuous service above 250°C, tensile strength rivaling aluminum at one-sixth the weight, and chemical resistance that survives autoclaves, jet fuel, and concentrated acids. But these same properties that make PEEK invaluable in aerospace, medical implants, and oil & gas also make it one of the most challenging materials to CNC machine correctly. The heat generated during cutting does not dissipate — it builds up in the chip and workpiece, causing melting, dimensional drift, and rapid tool wear.
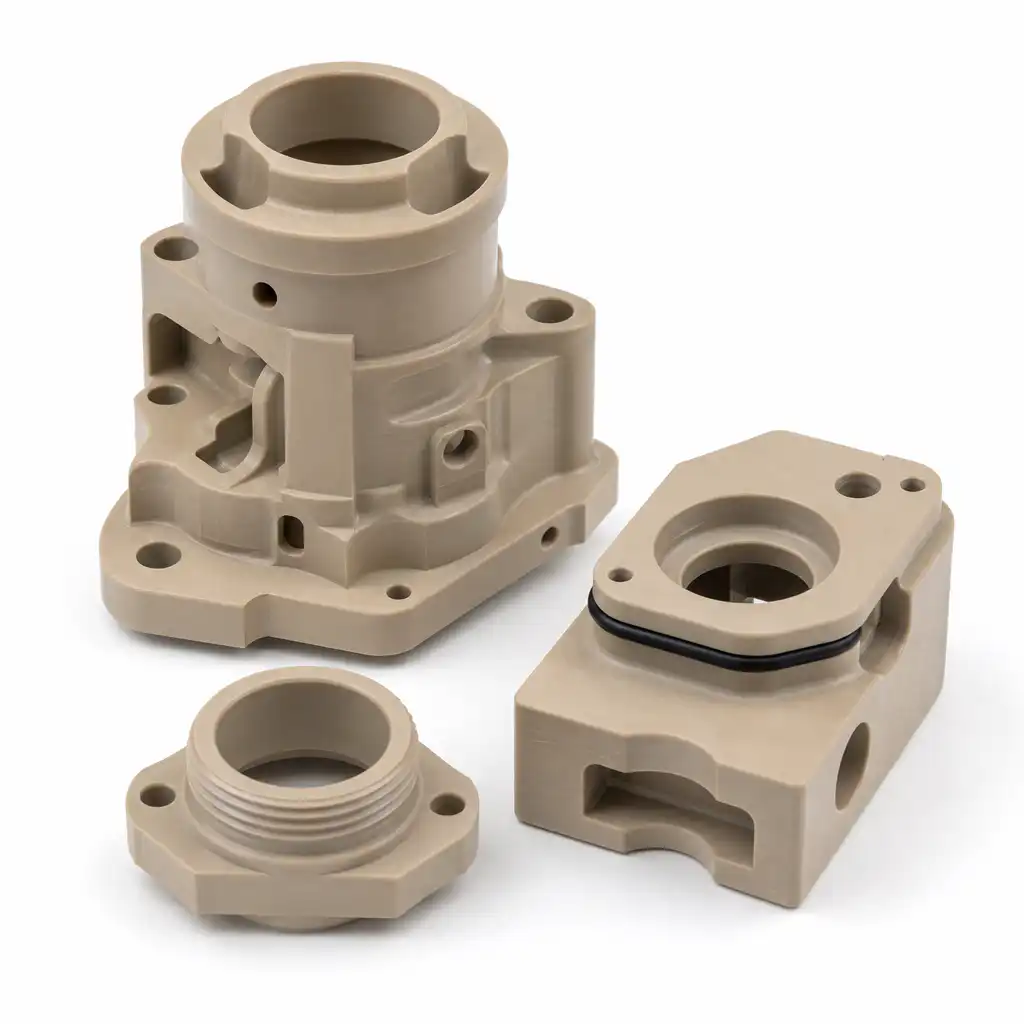
This guide covers PEEK machining parameters from our production floor: grade selection, feeds and speeds for each operation, the critical annealing step that most shops skip, and the tooling choices that make the difference between a $500 scrapped part and a flight-ready component.
PEEK Grades: Choosing the Right Variant for Machining
Unfilled PEEK (natural): The baseline. Tensile 95-100 MPa, excellent machinability (best surface finish), used for medical implants and seals. Machines similarly to brass — continuous chips, low tool wear. PEEK-GF30 (30% glass fiber): Stiffer (flex modulus 6 GPa vs 3.7 GPa for unfilled) but highly abrasive. Tool life drops 50-70% versus unfilled PEEK; carbide tools wear in 15-30 minutes of continuous cutting. PEEK-CF30 (30% carbon fiber): Highest stiffness and strength (tensile 220 MPa) but maximum abrasiveness. Requires diamond-coated tooling for production runs. Carbon fiber also makes the material electrically conductive — relevant for semiconductor applications.
Feeds and Speeds for CNC PEEK
| Operation | Tool | Speed (SFM) | RPM (6mm dia.) | Feed (mm/min) | DOC (mm) | Coolant |
|---|---|---|---|---|---|---|
| Roughing | 3-flute carbide | 150-300 | 8,000-12,000 | 600-1,200 | 1.5-3.0 | Flood / high-pressure |
| Finishing | 3-flute carbide | 200-400 | 10,000-15,000 | 300-600 | 0.2-0.5 | Flood coolant |
| Drilling | Carbide twist, 118 deg | 80-150 | 3,000-6,000 | 100-200 | Peck 2-3mm | Through-coolant if 5xD+ |
| Threading | Carbide thread mill | 100-150 | 5,000-8,000 | Helical | 0.1-0.2/pass | Flood lubricant |
| Slotting | 3-flute carbide | 120-200 | 6,000-10,000 | 400-800 | 0.5-1.0 | Trochoidal path + flood |
The plastic CNC machining guide covers drawing, stock and machining considerations alongside these PEEK-specific settings.
The Critical Annealing Step
PEEK accumulates significant internal stress during machining. The outer skin heats and expands while the core stays cool — as the part cools, this differential creates residual stresses that can cause warpage of 0.05-0.2 mm over the following days, or immediate cracking in thin-walled sections. Annealing protocol: Heat to 200°C (for unfilled) or 220°C (GF/CF grades) at 1°C/min, hold for 3 hours minimum (add 1 hour per 25 mm of thickest section), then cool at 0.5°C/min to below 140°C before removing from oven. Skipping this step guarantees dimensional instability in tight-tolerance PEEK parts.
Define the required dimensions and inspection conditions with the plastic-part tolerance guide.
Design Rules for Machining PEEK
- Tool selection: carbide minimum, diamond preferred: For unfilled PEEK, sharp polished carbide (AlTiN or TiAlN coated) runs 30-60 minutes before dulling. For GF/CF grades, CVD diamond-coated carbide extends tool life 5-10x. PCD (polycrystalline diamond) inserts reach 10-20x carbide life in production environments. The premium on diamond tooling pays back after 50-100 parts.
- Rigid fixturing with thermal compensation: PEEK expands at 47-55 x 10^-6 / °C — roughly 2x aluminum and 5x steel. A 100 mm part machined at 40°C (warm from cutting) shrinks 0.15-0.20 mm when measured at 20°C. Machine to nominal + thermal allowance, or machine in temperature-controlled coolant to keep the part at 20±2°C.
- Chip evacuation is everything: PEEK chips are tough, stringy, and do not break easily. They wrap around tools and re-cut, causing surface defects. Use high-pressure through-tool coolant (70+ bar) for deep holes, or peck drilling cycles with full retraction. For milling, compressed air at 6+ bar directed at the cut zone clears chips effectively for unfilled grades.
- Minimum wall thickness 1.0 mm: Below 1.0 mm, PEEK walls deflect under cutting pressure and produce chatter marks. For unsupported walls over 15 mm tall, increase minimum to 2.0 mm. Thin floors below 0.5 mm risk blowing through — the material softens at the cutting zone before the tool completes the pass.
- Threads: coarse pitch, never tap: Thread mill all PEEK threads. Taps bind and tear the material, producing rough, weak threads. Minimum thread size: M2 (M3 preferred). Depth limit: 2x diameter. Coarse pitch reduces the number of thin thread crests that crack under load. For structural threads, use helical inserts — the PEEK holds the insert; the insert holds the bolt.
- Post-machining inspection after full cool-down: Wait 24 hours after machining (or 4 hours after annealing) before final inspection. PEEK creeps slightly as residual stress relaxes — a part that measures in-tolerance fresh off the machine may be 0.03-0.08 mm out the next morning. For critical aerospace and medical parts, this waiting period is mandatory.
For geometry that needs access from several directions, compare the options in the multi-axis machining guide.
Industry Application Matrix
| Industry | Typical Parts | Material/Grade | Key Requirement |
|---|---|---|---|
| Aerospace | Brackets, bushings, seals, cable management | PEEK-CF30 or unfilled | FST (flame/smoke/toxicity) certified; -55 to +260°C range |
| Medical Implants | Spinal cages, dental abutments, trauma plates | Unfilled implant-grade PEEK | ISO 10993 biocompatibility; radiolucent for imaging |
| Oil & Gas | Seals, backup rings, electrical connectors | Unfilled or PEEK-GF30 | NORSOK M-710; H2S, CO2, and methanol resistance |
| Semiconductor | Wafer handling, test sockets, chamber components | PEEK-CF30 (ESD-safe) | Low outgassing; static dissipative (under 10^6 ohm/sq) |
For a PEEK power-transmission component, the plastic gear manufacturing guide covers the gear-specific design and quotation inputs.
Cost Decision Framework
Material cost: Unfilled PEEK rod/plate: $80-150/kg. PEEK-GF30: $90-170/kg. PEEK-CF30: $120-250/kg. This is 20-40x the cost of aluminum and 8-15x the cost of PA66. A single 100x100x25 mm plate costs $30-60 in material alone.
Machining cost: PEEK machines at ~50% of aluminum speed due to lower feeds and frequent tool changes. Diamond tooling adds $80-200 per tool but saves 5-10 tool changes per shift. Annealing adds 4-6 hours to lead time and $15-40 in oven cost per batch.
Decision rule: Machined PEEK only makes economic sense when: (a) quantity is 1-200 pcs (injection molding PEEK requires $25K-50K mold + $80-150/kg resin), (b) the part needs the combination of 250°C+ service, chemical resistance, and biocompatibility that no cheaper material offers, or (c) the cost of failure exceeds 100x the material premium — as in aerospace, medical implants, and deep-sea oil equipment.
Common Defects and Solutions
| Defect | Appearance | Root Cause | Solution |
|---|---|---|---|
| Surface melting / smearing | Glossy, melted patches on machined surface | Insufficient cooling; feed too slow for RPM | Increase flood coolant flow; raise feed 20% or reduce RPM to keep chip thickness adequate |
| Dimensional drift | Part measures out of tolerance 24h later | Residual stress from machining without annealing | Anneal per protocol (200°C/3h/slow cool); measure after cool-down |
| Chatter / poor surface | Visible wave pattern or roughness on surface | Tool stickout too long; insufficient fixturing rigidity | Reduce stickout below 4x diameter; add jack screws or vacuum fixture support |
| Rapid tool wear (GF/CF) | Cutting edge rounding after under 15 min cutting | Glass/carbon fiber abrading carbide tool edge | Switch to CVD diamond-coated or PCD tooling; reduce speed 15% for GF/CF |
Frequently Asked Questions
How does machining PEEK compare to machining aluminum?
PEEK machines at roughly 50% of aluminum speeds due to its lower thermal conductivity (0.25 W/mK vs 120+ W/mK for aluminum) — heat stays in the cut zone rather than dissipating through the chip. Feeds are 30-50% of aluminum rates. Tooling costs more: diamond-coated or PCD tools are strongly recommended versus standard carbide for aluminum. Surface finishes of Ra 0.4-0.8 μm are achievable with sharp tools — comparable to aluminum but requiring more careful parameter selection. The key difference is thermal management: aluminum carries heat away in the chip; PEEK requires the coolant to do all the work.
Does PEEK require annealing after machining?
Yes — this is not optional for tight-tolerance parts. PEEK accumulates internal stress during machining from the thermal gradient between the cutting zone (locally reaching 200°C+) and the cool core. Without annealing, parts warp 0.05-0.2 mm over 24-72 hours as stress relaxes. The standard protocol: heat to 200°C (unfilled) at 1°C/min, hold 3 hours minimum, cool at 0.5°C/min to below 140°C. Skipping this step virtually guarantees dimensional instability in parts with thin walls, deep pockets, or tolerances tighter than ±0.1 mm.
What are the best cutting tools for PEEK?
For unfilled PEEK: Sharp polished carbide with AlTiN or TiAlN coating, 3-flute end mills for milling, 118° point angle for drilling. For PEEK-GF30: CVD diamond-coated carbide extends tool life 5-10x over uncoated carbide. For PEEK-CF30: PCD (polycrystalline diamond) inserts or CVD diamond-coated end mills are required for production — standard carbide dulls in 10-15 minutes. Avoid TiN coatings — they have higher friction against PEEK than AlTiN/TiAlN. Tool cost: $25-60 (carbide) vs $80-200 (diamond-coated) vs $150-400 (PCD insert).
How does PEEK compare to PTFE (Teflon) for machined parts?
PEEK is stronger, stiffer, harder, and more temperature-resistant than PTFE — but 5-10x more expensive and requires more careful machining. Tensile: PEEK 95-100 MPa vs PTFE 20-30 MPa. Max service: PEEK 250°C vs PTFE 260°C (similar). Wear: PEEK has 10x better wear resistance. PTFE’s advantage is its extremely low friction coefficient (0.05-0.10 vs 0.30-0.38 for PEEK) and zero moisture absorption. Choose PEEK for structural, load-bearing applications; PTFE for seals, bearings, and low-friction surfaces where strength is secondary. The two are complementary, not competitive — many assemblies use PEEK for the structural body and PTFE for the sealing element.
Related Reading
Request a PEEK Machined-Part Review
For PEEK plastic machining of sealing, wear, structural or insulating components, share the drawing and operating conditions. Nylon Plastic can review the exact stock grade, machining sequence and dimensional acceptance before quotation.
What should a PEEK CNC machining quotation include for a critical component?
Specify the exact unfilled or reinforced grade, stock form, critical fits, load, temperature and inspection condition. Identify sealing, bearing or electrical surfaces and any approved material alternative. Ask the quote to state machining, deburring, cleaning, material records and dimensional inspection separately; a printed prototype cannot automatically validate the performance of a part cut from PEEK stock.
- Identify who supplies the stock and the required manufacturer, grade and lot records. State whether a reinforced or bearing grade, alternative source or customer-supplied stock is permitted.
- Define measurement temperature, part age, restraint and stability checks, plus any agreed stress-relief stage. Specify cleaning, contact-surface protection and packaging requirements for the actual end use.
- Provide prototype and repeat quantities, destination and timing. Separate stock, machining, stabilization, secondary operations and inspection; approve a production-intent sample against the controlled drawing.
Manufacturing and delivery:
- Precision Manufacturing: 30+ CNC & injection molding cells under one roof
- ISO 9001:2015 Certified: Certified quality system, full inspection reports
- 15-25 Day Lead Time: Fast turnaround with expedited options available
- Global Shipping: Air & sea freight to North America, Europe, Asia
A generic PEEK temperature or strength value is not a part qualification. For an existing critical application, confirm the approved grade, drawing and test requirements before changing the material source or manufacturing route.